Build the manufacturing release pack for each finished assembly or lot
For production managers, planners and plant leaders · Compare approaches
TL;DR — what you’ll learn
- Do not compile customer release documentation by manually copying PDFs into a shipment folder at dispatch time; bind every required test report, material certificate, as-built drawing revision, and quality release sign-off to the exact serial number or finished lot ID inside the ERP/QMS release pack before handing the unit over to logistics.
- Validate three identity gates for every packed unit: As-Built Configuration & Revision Match (unit serial/lot matches the authorised engineering revision on the order), Test & Inspection Provenance (the attached test certificate records the exact serial/lot and passes all specification limits), and Authorised Quality Release (any open nonconformance or concession is formally closed or customer-approved).
- Support controlled partial releases when one unit in a multi-unit order has a missing or mismatched certificate—holding only the affected serial in Release Pack Incomplete while allowing fully evidenced units to proceed to packing and logistics handover.
- In an illustrative four-panel order (SO-2026-8840, Serials PNL-26-401 through PNL-26-404), automated unit-to-document verification catches that dielectric test certificate HV-2026-112 attached to PNL-26-403 actually belongs to an earlier build (PNL-26-389 under Rev B instead of Rev C), blocking PNL-26-403 before packing while releasing the 3 verified panels (75.00% of the order) with complete 18-document evidence lineage.

Illustrative manufacturing inspection room and machine shop floor; not a client facility.
In engineered equipment, switchgear, pressure-vessel, and precision component manufacturing, a finished assembly is not commercially deliverable until its manufacturing release documentation pack—often called a Manufacturing Record Book (MRB), Certificate of Conformance (CoC) pack, or end-of-line quality dossier—matches the physical unit sitting on the packing floor. When quality or dispatch clerks assemble that pack manually by dragging PDFs from shared network drives just before the truck arrives, two expensive failures occur: a unit ships with a test report belonging to a different serial number or an obsolete drawing revision (triggering customer quarantine, rejection, or payment hold), or an entire multi-unit order is delayed because one unit's calibration or test record is still awaiting sign-off.
The core operational decision for quality assurance, manufacturing engineering, and finished-goods handover teams is to govern a serial- and lot-indexed manufacturing release pack as an explicit gate before logistics handover. This workflow resolves the manufacturing identity, as-built revision, and test-certificate lineage of each finished unit; vehicle scheduling, dock slot booking, e-Way bill generation, and carrier bills of lading remain separate downstream logistics workflows.
Why manual dispatch-folder compilation lets mismatched certificates slip through
When release documentation is treated as an administrative attachment added at the shipping desk rather than a structured manufacturing record, three structural gaps emerge:
- Order-level attachments hide serial-level mismatches: If a customer order calls for four identical motor-control panels (
PNL-26-401toPNL-26-404), attaching four PDF test reports to the sales-order header does not prove that each PDF covers the right panel, or that a reworked subassembly insidePNL-26-403was re-tested after component replacement. Traceability standards such as the GS1 Global Traceability Standard emphasise that finished-item identifiers must maintain an unbroken link to the specific transformation and inspection events performed on that exact physical instance. - Engineering revision drift between quotation, build, and certificate: As documented in Microsoft's engineering change management FAQ on product versioning in transactions, recording an engineering version on a master BOM is distinct from enforcing that exact version across every shop-floor transaction and inspection record. If a customer order requires wiring schematic
DWG-MCC-900 Rev C, but the final routine test was executed and signed againstRev Bon the shop floor, a manual clerk checking only "is a test report present?" will pass the defective dossier. - All-or-nothing order holds paralyse finished-goods handover: Without unit-level release-pack status, a missing heat-treatment chart or dielectric test signature on one unit either stalls all units on the production order or tempts staff to release the whole lot on a verbal promise to "email the PDF tomorrow."
In quality inspection workflows such as ERPNext's Quality Inspection module, outgoing inspection records link a specific item, batch, or serial number to measured parameters and an explicit Accepted or Rejected status. Extending that discipline to the complete release pack ensures that packing and handover consume verified system states rather than unindexed PDF filenames.
Unit-to-evidence matrix and partial-release governance
Every finished unit or lot must clear a structured Release Pack Manifest defined by the product's quality plan before its inventory status transitions from FG_WIP_PACKING to FG_RELEASED_FOR_LOGISTICS:
Scroll horizontally to see all columns.
| Evidence category in release pack | Required matching keys on document | Automated system validation rule | Exception handling if missing or mismatched | Accountable owner |
|---|---|---|---|---|
| 1. As-Built Identity & Revision Record | Serial_ID / Lot_ID + Item_Code + As_Built_Rev |
As_Built_Rev on completed work order must equal Required_Rev on customer order line (or link to an approved customer deviation) |
Block unit pack completion; route revision discrepancy to Manufacturing Engineering & QA | Manufacturing engineer & QA release lead |
| 2. Subassembly & Material Genealogy | Parent_Serial_ID → Child_Serial_ID / Heat_Lot_ID + Mill_Test_Cert_ID |
Every critical serialized component or raw-material heat lot installed in the unit must have an Accepted incoming inspection & certificate link |
Flag specific missing component certificate; verify against assembly serial genealogy | Quality assurance & stores traceability owner |
| 3. Final Routine / Functional Test Report | Test_Cert_ID + Tested_Serial_ID + Test_Timestamp + Tested_Against_Rev |
Tested_Serial_ID == Unit_Serial_ID, Tested_Against_Rev == As_Built_Rev, and Test_Timestamp > Last_Rework_Timestamp |
Reject stale or wrong-serial test certificate (ERR_SERIAL_OR_REV_MISMATCH); require re-test or correct certificate upload |
Test-bay supervisor & QC inspector |
4. Certificate of Conformance (CoC) & Final Release |
CoC_ID + Release_Pack_Manifest_SHA256 + QA_Approver_ID |
Generated only when Categories 1–3 are 100% complete (6/6 required documents verified) and zero open NCRs exist on the serial |
Allow partial order release for verified serials if customer contract permits partial handover; hold unverified serial in quarantine | Authorised Quality Release Signatory |
Serial-linked manufacturing release pack verification and partial handover workflow
Follow the workflow below, or open its complete text version.
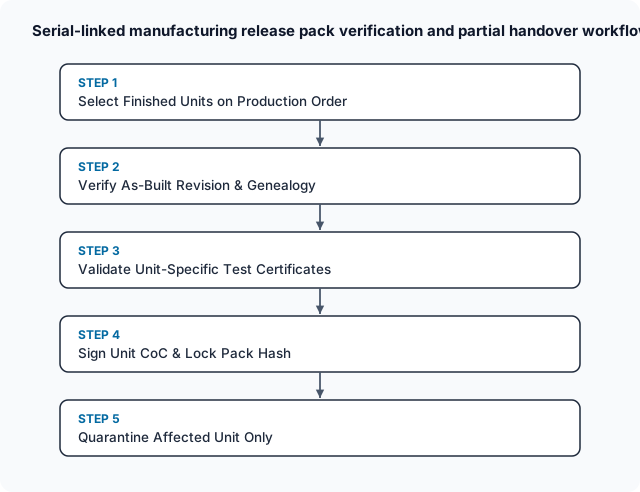
Read the complete workflow as text
- Select Finished Units on Production Order → Verify As-Built Revision & Genealogy
- Verify As-Built Revision & Genealogy → Validate Unit-Specific Test Certificates
- Validate Unit-Specific Test Certificates → Sign Unit CoC & Lock Pack Hash
- Sign Unit CoC & Lock Pack Hash → Quarantine Affected Unit Only
Worked example: Catching a wrong-serial test report across a four-panel order (SO-2026-8840)
All order numbers, panel serials, drawing revisions, and certificate identifiers below are illustrative examples constructed to show how unit-level release-pack validation prevents shipping an unverified assembly while preserving partial release for compliant units.
Suppose an electrical switchgear manufacturer completes production order WO-2026-5510 for customer order SO-2026-8840, comprising four 11 kV vacuum circuit-breaker control panels: Serials PNL-26-401, PNL-26-402, PNL-26-403, and PNL-26-404.
1. Required release-pack specification (6 documents per panel = 24 documents total)
Under the customer-approved quality plan, every individual panel serial requires 6 verified records before it can receive its signed Certificate of Conformance (CoC) and move to the dispatch staging bay (4 panels × 6 documents = 24 total document links):
- As-Built GA & Wiring Drawing Record matching approved order revision
DWG-VCB-11K-Rev-C. - Primary Busbar Copper Mill Test Certificate (
MTC) linked to the copper heat lot installed in that panel. - Vacuum Interrupter & Protection Relay Serial Genealogy Record matching the installed sub-serials.
- Point-to-Point Wiring & Torque Inspection Record signed by QC.
- High-Voltage Dielectric Withstand (
Hi-Pot,28 kV AC / 60 s) & Contact Resistance Test Certificate bearing the exact panel serial number and tested againstRev C. - Final Quality Release & Certificate of Conformance (
CoC) signed after items 1–5 pass.
2. Two defects uncovered in PNL-26-403 during release-pack compilation
When the test-bay clerk uploads the test certificates for the four panels, the automated release-pack matrix evaluates all 24 document links (6 per serial) and flags two critical errors on Serial PNL-26-403:
- Error 1 (Wrong serial & obsolete drawing revision on uploaded Dielectric Test Report): For
PNL-26-403, the clerk accidentally uploaded PDF test certificateHV-2026-112. The structured metadata header ofHV-2026-112recordsTested_Serial_ID = PNL-26-389(a panel from an earlier September production batch) andTested_Against_Rev = DWG-VCB-11K-Rev-B(whereasSO-2026-8840requiresRev C, which added an arc-fault trip supervision relay on terminal blockTB-14). - Error 2 (Post-rework test timestamp violation on
PNL-26-403): Even when the clerk locates the preliminary test record forPNL-26-403(HV-2026-148, recorded at09:40 ISTon19 October 2026), the unit's assembly serial genealogy shows that protection relayREL-OC-03insidePNL-26-403failed functional checkout at11:15 ISTand was replaced under rework stepRWK-403-01at13:20 ISTon19 October 2026:Test_Timestamp (09:40 IST) - Last_Rework_Timestamp (13:20 IST) = -220 minutes (-3 hours 40 minutes)Because the test timestamp precedes the component replacement by220 minutes, the pre-rework test certificate is invalidated;PNL-26-403requires a fresh post-rework dielectric and secondary-injection test againstRev C.
3. Unit-to-evidence reconciliation matrix across the four panels
By evaluating release-pack completeness at the individual serial level rather than the order header, the system cleanly separates the three compliant panels from the single non-compliant panel:
Scroll horizontally to see all columns.
| Panel Serial ID | Required Drawing Rev (Rev C) |
Busbar MTC & Sub-Serial Genealogy (2 docs) |
Wiring & Torque Inspection (1 doc) |
Dielectric & Functional Test Cert (1 doc) |
Post-Rework Timestamp Check (t_test > t_rework) |
CoC & Release Pack Status (Docs Verified) |
Handover Disposition |
|---|---|---|---|---|---|---|---|
PNL-26-401 |
Rev C (Match) |
MTC-Cu-881 + GEN-401 (Verified) |
INSP-W-401 (Accepted) |
HV-2026-146 (Serial = PNL-26-401, Rev C) |
No rework (t_test = 19 Oct 08:30) — Pass |
6 / 6 Verified (PACK-401-OK) |
Released to Logistics Handover |
PNL-26-402 |
Rev C (Match) |
MTC-Cu-881 + GEN-402 (Verified) |
INSP-W-402 (Accepted) |
HV-2026-147 (Serial = PNL-26-402, Rev C) |
No rework (t_test = 19 Oct 09:05) — Pass |
6 / 6 Verified (PACK-402-OK) |
Released to Logistics Handover |
PNL-26-403 |
Rev C (Match) |
MTC-Cu-881 + GEN-403-R1 (Relay replaced 13:20) |
INSP-W-403 (Accepted) |
Blocked: Uploaded HV-2026-112 is for PNL-26-389 (Rev B); prior HV-2026-148 (09:40) predates 13:20 relay replacement |
Fail (-220 min stale test) |
4 / 6 Verified (HOLD-PACK-403) |
Quarantined at Test Bay (Blocked from Packing) |
PNL-26-404 |
Rev C (Match) |
MTC-Cu-882 + GEN-404 (Verified) |
INSP-W-404 (Accepted) |
HV-2026-149 (Serial = PNL-26-404, Rev C) |
No rework (t_test = 19 Oct 10:15) — Pass |
6 / 6 Verified (PACK-404-OK) |
Released to Logistics Handover |
Order Summary (4 Serials) |
4 / 4 As-Built Rev C |
8 / 8 Genealogy & MTC Docs |
4 / 4 Inspection Docs |
3 / 4 Valid Test Certs (1 Blocked) |
3 / 4 Pass (1 Requires Re-Test) |
22 / 24 Total Links Verified (91.67%) |
3 / 4 Panels (75.00%, 18/18 docs) Released; 1 / 4 (25.00%) Held |
4. Operational impact of serial-level gating
- Zero defective documentation reaches the customer: Blocking
PNL-26-403prevents shipping a₹14,50,000switchgear panel with another unit'sRev Btest certificate—avoiding a formal site-acceptance rejection and a manufacturing invoice dispute hold on collection. - Controlled partial handover preserves schedule: Because customer contract
SO-2026-8840permits partial lot handover for Substation Bay 1 (PNL-26-401,PNL-26-402,PNL-26-404), the quality lead signs partial release manifestREL-MAN-8840-Acovering the3verified panels (18 / 18required documents verified, cryptographic bundle hashSHA-256locked) whilePNL-26-403returns to the test bay for its45-minutepost-rework dielectric and relay test (HV-2026-155againstRev C). - Clear boundary with cure/test holds and logistics execution: Just as precast and cementitious products require cure age and test status clearance before release, finished assemblies require a complete release document pack before logistics handover. Once a serial is marked
FG_RELEASED_FOR_LOGISTICS, transport planning, carrier allocation, loading readiness, and transit documentation are managed by the logistics workflow.
Observable acceptance tests for manufacturing release document packs
Verify these three acceptance tests in your ERP/QMS environment before go-live:
ACT-M077-01(Serial and revision mismatch block on test certificate attachment): Attempt to complete the release pack for unitPNL-26-403(As_Built_Rev = Rev C) by linking a test certificate record whoseTested_Serial_IDisPNL-26-389or whoseTested_Against_RevisRev B. Pass condition: The system rejects the link (Error: Certificate HV-2026-112 serial/revision [PNL-26-389 / Rev B] does not match target unit [PNL-26-403 / Rev C]) and blocksCoCgeneration forPNL-26-403.ACT-M077-02(Automatic invalidation of test records predating component replacement or rework): Log a component replacement (RWK-403-01at13:20 IST) on serialPNL-26-403after its final test record (HV-2026-148at09:40 IST) was already uploaded. Pass condition: The release pack automatically changesHV-2026-148status fromVerifiedtoSuperseded by Post-Test Rework (-220 min)and revertsPNL-26-403fromReady for ReleasetoQuarantined — Re-Test Required.ACT-M077-03(Unit-level partial release without leaking unverified serials into packing manifests): Execute a partial release on a4-unitorder where3serials (PNL-26-401, 402, 404) have6/6verified documents and1serial (PNL-26-403) has4/6. Pass condition: The packing and handover manifest includes only the3verified serials (18document links) and physically blocks printing a packing label orCoCforPNL-26-403.
Next actions for quality, manufacturing engineering, and handover teams
To eliminate manual dispatch-folder errors and ensure every shipped unit carries verified as-built evidence, take these four numbered actions:
- Define a structured Release Pack Document Template per product family in QMS/ERP: Replace free-form email checklists with a mandatory digital manifest specifying the exact certificate types, drawing revision fields, and inspection records required per serial or batch.
- Capture
Tested_Serial_ID,Tested_Against_Rev, andTest_Timestampas structured fields on every test record: Stop uploading unindexed PDF scans; require test-bay technicians to select the exact serial number and drawing revision in the QMS/ERP inspection record when attaching test output. - Configure an automatic timestamp check between rework/genealogy updates and final test certificates: Ensure that any component swap or rework logged on a serialized assembly after its final inspection timestamp automatically invalidates the prior release sign-off (
ACT-M077-02). - Gate finished-goods packing labels on
Release Pack Verifiedstatus: Configure the packing station printer so a logistics handover label and Certificate of Conformance (CoC) can only be printed for serials or lots whose release-pack manifest is100%complete (6/6required records verified).
Compare this workflow with your current setup
Share the step that takes the most manual work, the systems involved and the exceptions your team handles. That gives us a concrete starting point for comparing approaches.
Sources and further reading
Sources checked 15 October 2026. Worked examples and workflow diagrams are original illustrations, not reported client results.


