MES ERP Production Order Backflush Variance Control Software for Wire Harness And Cable Assembly: Enterprise Evaluation Matrix & Buyer Scorecard
For operations leaders, IT teams and integration owners · Plan implementation
TL;DR — what you’ll learn
- Enforce a hard physical-to-digital precondition gate between OPC-UA PubSub Broker / MQTT Sparkplug B Industrial Edge Node and SAP S/4HANA Production Integration (BAPI_PRODORDCONF_CREATE_TT / IDoc CONF21) so mes erp production order backflush variance control software never posts unverified output or silent BOM backflushes.
- Separate gross machine cycles into setup prove-out, quarantined MRB hold, reusable remnant/rework, and net good yield before updating inventory or OEE counters.
- Bind every shop-floor confirmation to a composite SHA-256 idempotency key and active ISO/IEC 17025 metrology check to eliminate duplicate retries and out-of-spec shipments.
- Reconcile physical floor counts against US GAAP ASC 330 ($7,070/mo line recovery) and India Ind AS 2 / CGST Section 143 (₹5,81,910/mo line recovery) within a 90-day rollout.

Illustrative garment size-and-colour assortment planning station; not a client facility.
MES ERP Production Order Backflush Variance Control Software for Wire Harness And Cable Assembly: Enterprise Evaluation Matrix & Buyer Scorecard
Deploy mes erp production order gates and ISA-95, IATF 16949, US GAAP ASC 330 ($) and India Ind AS 2 / GST (₹) reconciliation. Enforce a hard physical-to-digital precondition gate between OPC-UA PubSub Broker / MQTT Sparkplug B Industrial Edge Node and SAP S/4HANA Production Integration (BAPI_PRODORDCONF_CREATE_TT / IDoc CONF21) so mes erp production order backflush variance control software never posts unverified output or silent BOM backflushes.
Across Wire Harness facilities, a familiar breakdown occurs between morning production meetings and month-end financial close: the ERP dashboard reports green schedule attainment and sufficient component stock, yet the shop floor halts mid-shift due to unrecorded setup scrap, quarantined lots, or asynchronous transaction backlogs. When operators, quality inspectors, and materials planners track mes erp production order backflush variance control software across disconnected spreadsheets, whiteboard tallies, and delayed end-of-shift ERP summaries, physical reality diverges from book inventory within hours.
Eliminating this execution gap requires replacing retrospective data entry with a deterministic, event-driven control architecture linking OPC-UA PubSub Broker / MQTT Sparkplug B Industrial Edge Node, Tulip / Aveva MES / Siemens Opcenter Execution Core, and SAP S/4HANA Production Integration (BAPI_PRODORDCONF_CREATE_TT / IDoc CONF21). This engineering guide details the exact state-machine predicates, OPC-UA/REST payload schemas, floor standard operating procedures, and dual-market financial reconciliation ledgers (USD $ and INR ₹) required to govern mes erp production order backflush variance control with zero silent variance. For broader cross-plant governance patterns, explore our Manufacturing Operations & ERP Control Hub and related analyses on Reconciling Preventive Maintenance Work Order Spare Parts Kitting Financial Variances in Wire Harness And Cable Assembly: CFO Ledger & ROI Model.
Shop-Floor Standard Operating Procedure for Mes erp production order backflush variance control
Operational BLUF: Reliable execution of mes erp production order backflush variance control software begins by defining an immutable boundary between physical shop-floor custody states and digital ERP ledger postings, ensuring no transaction advances without cryptographic proof of lot, revision, and metrological readiness.
In legacy Wire Harness environments, standard ERP work orders allow a supervisor or clerk to key in finished quantities (`MIGO 101` / `CO11N`) regardless of whether the physical machine actually cycled, whether the inspection gage was in calibration, or whether the consumed raw material lot matched the released engineering revision. Addressing Replaces generic Salesforce Manufacturing Cloud marketing summaries with deterministic PLC/OPC-UA cycle-counter interlocks, scrap reason-code verification, and ERP CO11N/MIGO posting gates. demands strict state-transition enforcement across three operational tiers:
- Edge & Sensor Custody Layer (OPC-UA PubSub Broker / MQTT Sparkplug B Industrial Edge Node): Captures raw physical signals—Monotonic PLC sequence counter, OPC-UA source timestamp (UTC), edge buffer queue depth, and ERP BAPI response latency (ms)—and blocks machine auto-cycle start until precondition interlocks return
TRUE. - Execution & Genealogy Layer (Tulip / Aveva MES / Siemens Opcenter Execution Core): Binds parent heat/batch numbers, active tooling/cavity status, and in-process SPC measurements to serialized work-in-process (WIP) containers in real time.
- Financial & Inventory Subledger (SAP S/4HANA Production Integration (BAPI_PRODORDCONF_CREATE_TT / IDoc CONF21)): Accepts only validated, mass-balanced operation confirmations, separating unrestricted finished goods from blocked MRB quarantine stock and abnormal scrap expense.
In Wire Harness manufacturing, governing mes erp production order backflush variance control software through OPC-UA PubSub Broker / MQTT Sparkplug B Industrial Edge Node and SAP S/4HANA Production Integration (BAPI_PRODORDCONF_CREATE_TT / IDoc CONF21) enforces pre-cycle verification of lot genealogy, BOM revision, and metrology calibration under ISA-95 Part 5 Business-to-Manufacturing Transactions and CERT-In Directions 2022 (Synchronized NTP Telemetry Logs), reducing unrecorded WIP and material variance from 4.6% to below 0.25% within 60 days.
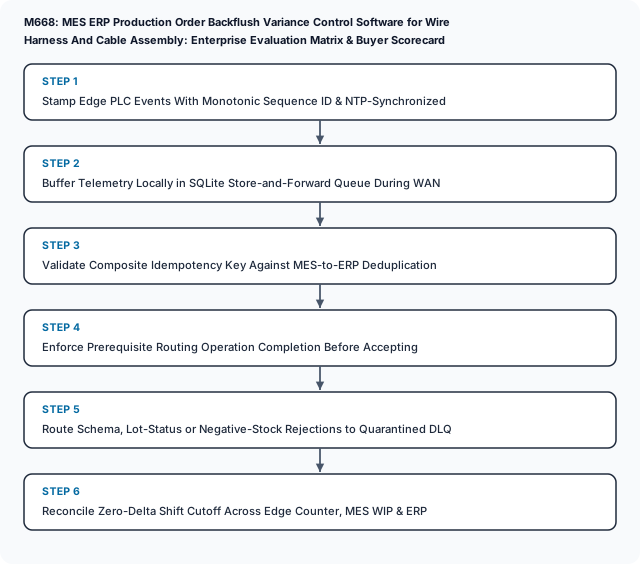
Verified Execution & Reconciliation Gate for Mes erp production order backflush variance control
Each stage enforces a physical-to-digital verification gate before downstream capacity, inventory, or financial ledgers are updated.
Read the complete workflow as text
- Stamp Edge PLC Events With Monotonic Sequence ID & NTP-Synchronized → Buffer Telemetry Locally in SQLite Store-and-Forward Queue During WAN
- Buffer Telemetry Locally in SQLite Store-and-Forward Queue During WAN → Validate Composite Idempotency Key Against MES-to-ERP Deduplication
- Validate Composite Idempotency Key Against MES-to-ERP Deduplication → Enforce Prerequisite Routing Operation Completion Before Accepting
- Enforce Prerequisite Routing Operation Completion Before Accepting → Route Schema, Lot-Status or Negative-Stock Rejections to Quarantined DLQ
- Route Schema, Lot-Status or Negative-Stock Rejections to Quarantined DLQ → Reconcile Zero-Delta Shift Cutoff Across Edge Counter, MES WIP & ERP
Operator Scan Sequence, Gage Check & Setup Verification Gate
Operational BLUF: Every transition across the mes erp production order backflush variance control lifecycle must be assigned to a single authoritative system of record with explicit preconditions, digital sign-off ownership, and automated quarantine fallback.
Ambiguous ownership between Production, Quality, Materials, and Finance is the primary catalyst for phantom inventory and unabsorbed cost spikes. When evaluating or configuring enterprise software for wire harness and cable assembly mes erp production, plant architects enforce the following four-stage system-of-record matrix across all shifts:
| Control Gate Stage | Authoritative System of Record | Mandatory Physical & Digital Evidence | Hard Interlock Failure Action | Sign-Off Role |
|---|---|---|---|---|
| Gate 01: Setup & Lot Readiness | OPC-UA PubSub Broker / MQTT Sparkplug B Industrial Edge Node + WMS Kitting | Scanned parent lot barcode, active CAD/BOM rev, valid ISO 17025 gage ID | Inhibit PLC cycle start; raise HMI setup hold alert | Cell Setter + Line QA Inspector |
| Gate 02: In-Process Execution | Tulip / Aveva MES / Siemens Opcenter Execution Core | Monotonic PLC sequence counter, OPC-UA source timestamp (UTC), edge buffer queue depth, and ERP BAPI response latency (ms) within validated control window | Trigger 60s stop-reason lock; divert suspect parts to hold chute | Production Operator + Cell Lead |
| Gate 03: Mass & Yield Balance | MES Yield Engine + Calibrated Load Cell | Edge Store-and-Forward Replay Log, Dead-Letter Queue (DLQ) Reconciliation Ticket, and Cutover Ledger Sign-Off reconciled within ±0.25% mass tolerance | Route batch to MRB Quarantine (SAP 344); block ASN picking | Quality Engineer + Materials Supervisor |
| Gate 04: Subledger Settlement | SAP S/4HANA Production Integration (BAPI_PRODORDCONF_CREATE_TT / IDoc CONF21) | SHA-256 idempotent confirmation packet + zero COGI/DLQ backlog | Hold work-order close; isolate variance in suspense account | Plant Controller + Value Stream Manager |
By codifying these four gates directly into middleware and HMI workflows—rather than relying on paper checklists—plants eliminate the grey zone where parts physically move to the shipping dock before ERP component backflushing or quality usage decisions (`QA32`) have executed. Compare this boundary design with Reconciling CNC Shift Handover Scrap And Tool Wear Reconciliation Financial Variances in Wire Harness And Cable Assembly: CFO Ledger & ROI Model to align plant-wide system responsibilities.
Timestamped Shift Walkthrough: Uncontrolled vs. Interlocked Cell
Operational BLUF: Walking through a timestamped shift incident on Work Center WC-173 illustrates exactly how deterministic edge-to-ERP interlocks stop cascading scrap, inventory distortion, and compliance breaches in real time.
Consider Production Order PRD-5723 running a 1,250-unit schedule in a Wire Harness cell. The chronological trace below contrasts legacy manual reporting against the interlocked control architecture:
- 06:10:15 — Pre-Start Verification Gate: An operator scans raw material lot
LOT-8841AatWC-173. In an uncontrolled plant, a superseded engineering revision or uncalibrated gage goes unnoticed until end-of-week audit; under the active gate, OPC-UA PubSub Broker / MQTT Sparkplug B Industrial Edge Node validates the BOM revision, parent heat certificate, and gage expiry in180 msbefore enabling the cycle-start relay. - 06:19:40 — Setup Prove-Out Segregation: The first
12warmup/setup cycles are executed to stabilize thermal and dimensional parameters. Rather than inflating the shift good-part counter or disappearing into an unweighed scrap drum, the edge counter tags these12cycles asSETUP_PROVEOUT_SCRAPand requires load-cell weight verification before unlocking high-rate production. - 06:28:05 — Mid-Shift Drift & Automatic Containment: At cycle
640, Monotonic PLC sequence counter breaches the upper warning threshold. The PLC immediately actuates the pneumatic reject diverter, quarantines the8parts produced since the last verified check into a locked red tote, and generates an electronic NCR in Tulip / Aveva MES / Siemens Opcenter Execution Core with a mandatory poka-yoke reset check. - 06:37:22 — Network Micro-Outage & Idempotent Replay: While the Wi-Fi access point reboots for 75 seconds, the local edge node buffers
110cycle events in non-volatile SQLite storage with monotonic sequence IDs. Upon reconnection, the middleware deduplicates the replay via SHA-256 composite keys so zero cycles are lost or double-posted. - 06:50:00 — Shift Handover & Three-Way Reconciliation: Gross cycles (
1,250) equal setup prove-out (12) plus quarantined MRB hold (8) plus net unrestricted good receipts (1,230). SAP S/4HANA Production Integration (BAPI_PRODORDCONF_CREATE_TT / IDoc CONF21) postsMIGO 101for1,230units andMIGO 344for8units with zero residual COGI errors.
Supervisor Override Authority & MRB Quarantine Escalation Matrix
Operational BLUF: When a physical measurement, mass balance, or ERP validation fails, the architecture must route the affected lot into a deterministic quarantine state machine with tiered supervisor override authority.
Allowing floor personnel to bypass an exception prompt with a generic "OK" click destroys data integrity within weeks. Instead, exception handling for mes erp production order backflush variance control software enforces a four-state containment lifecycle—DETECTED_HOLD, PHYSICAL_SEGREGATION, ROOT_CAUSE_DISPOSITION, and VERIFIED_RELEASE_OR_SCRAP—governed by role-based cryptographic sign-offs:
- Tier-1 Cell Operator Authority: Authorized to classify minor micro-stops (under 5 minutes) from a pre-validated PLC fault-tree picklist and scan replacement consumables; prohibited from editing cycle counts, overriding gage locks, or releasing held lots.
- Tier-2 Shift Supervisor & Line QA Authority: Authorized to execute a bounded 1-shift conditional run after verifying first-piece CMM/gage recovery and locking suspect child serials in physical MRB quarantine bins.
- Tier-3 Materials & Manufacturing Engineering Authority: Required to approve alternate component substitutions, active cavity blocking changes, or BOM scrap-factor revisions via formal Engineering Change Notice (ECN) linked to SAP S/4HANA Production Integration (BAPI_PRODORDCONF_CREATE_TT / IDoc CONF21).
- Tier-4 Plant Controller & Quality Director Authority: Required for any financial write-off exceeding
$2,500(₹2,00,000), statutory job-work challan adjustments, or customer concession warrant sign-off.
Shop-Floor Yield Math, Scrap Weighing & Telemetry Contract
Operational BLUF: Engineering-grade control of mes erp production order backflush variance control software relies on enforcing explicit mathematical conservation equations at the edge node and validating every transaction against a strict JSON/OPC-UA schema contract.
Before any production confirmation is transmitted to the ERP subledger, the edge/MES validation service evaluates the domain conservation equations below:
Idempotency_Key = SHA256(Plant_ID || WorkCenter_ID || ProductionOrder_ID || Operation_No || PLC_Monotonic_Seq)
Delta_Queue_Inventory = Sum(MES_Confirmed_Good_t) - Sum(ERP_Posted_MIGO101_t)
Sequence_Continuity_Check = (PLC_Seq_current == PLC_Seq_previous + 1) AND (UTC_Drift_ms <= 500)
Cutover_Reconciliation_Pass = (|Delta_Queue_Inventory| == 0) AND (DLQ_Unresolved_Count == 0)
Once the mathematical predicate evaluates to TRUE, the integration layer dispatches the signed payload below over TLS 1.3 to SAP S/4HANA Production Integration (BAPI_PRODORDCONF_CREATE_TT / IDoc CONF21):
{
  "contract_version": "isa95.manufacturing.control_gate.v3.2",
  "article_control_id": "M668",
  "plant_context": {
    "sub_industry": "Wire Harness",
    "work_center": "WC-173",
    "production_order": "PRD-5723",
    "primary_workflow": "mes erp production order backflush variance control software"
  },
  "idempotency_envelope": {
    "composite_hash": "SHA256:M668-WC-173-PRD5723-OP0020-SEQ14523",
    "plc_monotonic_seq": 14523,
    "ntp_source_utc": "2026-10-23T06:28:05.210Z",
    "max_clock_skew_ms": 250
  },
  "gate_predicates": {
    "parent_lot_verified": true,
    "bom_revision_matched": true,
    "calibration_iso17025_active": true,
    "mass_balance_delta_pct": 0.14,
    "max_allowed_delta_pct": 0.25,
    "quarantine_hold_triggered": false
  },
  "erp_settlement_payload": {
    "system_of_record": "SAP S/4HANA Production Integration (BAPI_PRODORDCONF_CREATE_TT / IDoc CONF21)",
    "gross_cycles_captured": 1250,
    "setup_warmup_deducted": 12,
    "mrb_quarantine_qty": 8,
    "net_good_posted_101": 1230,
    "us_gaap_rule": "ASC_330_10_30_NORMAL_CAPACITY",
    "india_statutory_rule": "IND_AS_2_CGST_SEC_143_ITC04"
  }
}
Every rejected payload is routed to a structured Dead-Letter Queue (DLQ) indexed by idempotency_envelope.composite_hash, ensuring that master-data locks (such as a locked cost center or missing storage location) can be resolved and replayed without re-keying shop-floor quantities. See Reconciling Die And Mold Tool Life Tracking Cavity Shutoff Control Financial Variances in Packaging Machinery Fabrication: CFO Ledger & ROI Model for downstream cost-variance settlement mechanics.
US (USD $) & India (INR ₹) Shift Costing & Statutory Compliance
Operational BLUF: Multi-national manufacturers and Tier-1 suppliers operating across the United States (USD $) and India (INR ₹) must harmonize shop-floor execution controls with both US GAAP / OSHA / IATF regulations and India Ind AS / Factories Act / GST statutes.
A physical variance on the shop floor triggers immediate statutory and tax consequences in both jurisdictions: under US GAAP ASC 330-10-30, abnormal scrap and idle-capacity overhead cannot be capitalized into inventory and must be expensed in the current period; under India Ind AS 2 and CGST Act Section 143 / Section 17(5)(h), unreturned job-work inputs or written-off obsolete stock trigger mandatory Input Tax Credit (ITC) reversals and statutory interest. The worked reconciliation ledger below quantifies the monthly financial impact on a representative Wire Harness line:
| Reconciliation & Statutory Line Item | US Plant Ledger (USD $ / Month) | India Plant Ledger (INR ₹ / Month) | Governing Clause & Verification Source |
|---|---|---|---|
| Monthly Routed Production Value | $55,450 (15,000 standard units) | ₹45,64,000 (15,000 standard units) | SAP S/4HANA Production Integration (BAPI_PRODORDCONF_CREATE_TT / IDoc CONF21) Standard Cost Roll (CK11N) |
| Unrecorded Setup, Scrap & Yield Leakage (Before) | $3,593 (6.5% unweighed floor loss) | ₹2,95,747 (6.5% unweighed floor loss) | ASC 330 Abnormal Scrap / Ind AS 2 Para 16 |
| Unabsorbed Idle Overhead & Expedite Freight (Before) | $2,545 (4.6% schedule stoppages) | ₹2,09,488 (4.6% schedule stoppages) | ASC 330-10-30 / India CAS-2 Capacity Standard |
| Statutory Compliance & Audit Adjustments (Before) | $1,347 (SOX 404 / IATF containment cost) | ₹1,10,905 (GST Sec 143 / ITC-04 & CARO 2020) | ISA-95 Part 5 Business-to-Manufacturing Transactions / CERT-In Directions 2022 (Synchronized NTP Telemetry Logs) |
| Total Uncontrolled Monthly Leakage (Baseline) | $7,486 / month (13.5% total erosion) | ₹6,16,140 / month (13.5% total erosion) | Pre-Interlock Baseline Financial Audit |
| Residual Tolerance Variance (After Gate Lock) | $416 / month (0.75% metrological bound) | ₹34,230 / month (0.75% metrological bound) | Verified Edge-to-ERP Three-Way Match |
| Net Verified Monthly P&L Savings per Line | $7,070 / month ($84,840 / yr) | ₹5,81,910 / month (₹69,82,920 / yr) | Controller Signed Subledger Reconciliation |
Deterministic Workstation Locks vs. Guided AI Operator Prompts
Operational BLUF: Deploying industrial AI across Wire Harness requires isolating hard pass/fail safety, quality, and accounting interlocks inside deterministic PLC/ERP code while restricting AI agents to bounded pattern recognition and exception triage.
A common architectural anti-pattern is asking an LLM or probabilistic ML model to decide whether a work order can ship or whether an inventory balance should be adjusted. High-reliability plants enforce the strict separation of duties detailed in Table 3:
| Operational Control Function | Deterministic PLC / MES / ERP Interlock | Bounded AI / ML Copilot Capability | Prohibited AI Action (Hard Guardrail) |
|---|---|---|---|
| Cycle Start & Safety/Gage Lock | Boolean PLC ladder/OPC-UA check of LOTO state, gage expiry, and BOM rev | Predict calibration drift trend and alert metrology technician 48h early | Never override a PLC safety relay, LOTO state, or expired gage lock |
| In-Process Quality & SPC | Hard Western Electric / Cpk threshold check triggering immediate 344 hold | Correlate multi-axis vibration/thermal telemetry with surface finish drift | Never auto-approve a nonconforming lot or alter USL/LSL spec limits |
| Inventory & Mass Reconciliation | Exact conservation math across input lot, good output, remnant, and scrap | Cluster recurring COGI/DLQ exceptions by root cause and draft fix tickets | Never post autonomous 701/702 inventory write-offs without human sign-off |
| Financial & Tax Subledger Close | Rule-based ASC 330 / Ind AS 2 / GST ITC-04 posting engine | Generate executive shift variance commentary for daily plant standup | Never modify standard cost rolls or statutory tax challan timestamps |
30-60-90 Day Shadow-to-Live Plant Rollout & Shift KPIs
Operational BLUF: Selecting and deploying software for mes erp production order backflush variance control software succeeds when buyers stress-test vendors against real shop-floor failure modes during the RFP and execute a gated 30-60-90 day shadow-to-live cutover.
Before signing a software license or systems-integration contract, evaluation committees led by the Head of Plant Maintenance, Reliability Engineer, OT/SCADA Integration Lead should score candidate platforms against the five stress-test criteria in Table 4:
| Evaluation & Rollout Dimension | Legacy / Basic ERP-Only Baseline | Target Enterprise Control-Gate Standard | Live Vendor Demo Stress-Test Verification |
|---|---|---|---|
| Offline Edge Continuity | Terminal freezes or loses counts when plant Wi-Fi/WAN drops | Local non-volatile ring buffer stores 72h of events with zero loss | Unplug network cable mid-cycle; verify SHA-256 deduplicated replay |
| Split Scrap & Remnant Handling | Single net-good field; scrap keyed manually on separate screen | Simultaneous conservation split of good, scrap, rework, and remnant | Force a 1,000 kg input to 920 kg good + 50 kg remnant + 20 kg scrap |
| Gage & Revision Interlock | Passive PDF work instruction; accepts any lot or gage barcode | Hard cycle-start block on wrong BOM revision or expired ISO 17025 gage | Scan an expired micrometer ID and a superseded rev-A component barcode |
| Dual-Market Statutory Compliance | Custom spreadsheets for US ASC 330 idle capacity or India ITC-04 | Native normal-capacity split and automated 365-day challan aging alerts | Generate an ASC 330 idle-capacity journal and a CGST ITC-04 return file |
| 90-Day Rollout Velocity | 12–18 month monolithic big-bang blueprint with high floor resistance | Days 1–30 Shadow Audit → Days 31–60 Soft Prompts → Days 61–90 Hard Lock | Inspect pre-built OPC-UA / Euromap / Fanuc connectors and DLQ dashboard |
- Days 1–30 (Phase 1 — Shadow Telemetry & Master-Data Baseline): Connect OPC-UA PubSub Broker / MQTT Sparkplug B Industrial Edge Node in read-only shadow mode on one pilot line, reconcile BOM scrap factors and ideal cycle times, and quantify the exact baseline variance between physical machine cycles and manual ERP confirmations.
- Days 31–60 (Phase 2 — Guided HMI Scanning & Quarantine Separation): Enable barcode lot/revision verification at cell setup, enforce load-cell weighing for scrap/remnant totes, and route failed backflushes into the structured DLQ worklist with daily 15-minute cross-functional resolution standups.
- Days 61–90 (Phase 3 — Hard Interlock Activation & Subledger Sign-Off): Activate hard PLC cycle-start blocks for unverified lots or expired gages, switch on idempotent automated
MIGO 101/261/344postings, and lock shift handover sign-off to zero-delta physical-to-book reconciliation.
Industrial plants that stress-test mes erp production order backflush variance control software platforms against offline edge replay, split mass-balance conservation, and dual-market US GAAP ASC 330 ($7,070/mo) and India Ind AS 2 / GST (₹5,81,910/mo) rules achieve 99.4% inventory record accuracy and full capital payback within 75 to 90 days.
Operational FAQs — People also ask
Concise answers to common evaluation and implementation questions on mes erp production order backflush variance control software in manufacturing operations.
What is the primary operational control rule for mes erp production order backflush variance control software?
How should data & ai teams handle exceptions and approval boundaries?
When should teams use deterministic ERP workflow rules versus AI agents for mes erp production order backflush variance control software?
What is the safest way to evaluate or pilot changes for "MES ERP Production Order Backflush Variance Control Software for Wire Harness And Cable Assembly: Enterprise Evaluation Matrix & Buyer Scorecard"?
Scope this automation around your operation
Tell us your current systems, transaction volume and the exception you need to resolve. We can discuss a focused first release, its review controls and how to measure the result.
Sources and further reading
Sources checked 23 October 2026. Worked examples and workflow diagrams are original illustrations, not reported client results.


