Returnable Packaging & Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation
For procurement, stores and subcontract operations teams · Understand the problem
TL;DR — what you’ll learn
- Enforces closed-loop synchronization for Returnable Packaging and Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation (M144) across SAP LO-HU (Handling Unit Management), Returnable Packaging Account (RLAC / V_T685A), Movement Types 621/622 (Customer lending/return) and 541/542 (Vendor subcontracting dunnage), plus UHF RFID / QR gate-pass reconciliation.
- Governs shop-floor execution via the mathematical balance Required RTI Fleet Size = ceil((Daily_Part_Volume / Parts_per_Container) × Total_Turnaround_Cycle_Days × (1 + Peak_Variance_Buffer)); Unreturned Container Deposit Liability = max(0, Balance_at_Partner - Contractual_Float_Limit) × Replacement_Asset_Cost.
- Eliminates Treating returnable steel racks and vacuum-formed blisters as untracked overhead until emergency expendable cardboard purchases erode margin through real-time PLC/MES interlocks.
- Aligns dual-market compliance across GST Section 143 / Rule 45 and Circular 126/45/2019-GST delivery challa and AIAG B-16 / RC-14 Global Returnable Tire and Container RFID/barcode iden.

Illustrative factory raw-material stores and receiving counter; not a client facility.
Returnable Packaging & Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation
Implement returnable packaging management software with MES/ERP state interlocks, worked Indian INR reconciliation, and ISO 9001 / IATF 16949 audit governance. Enforces closed-loop synchronization for Returnable Packaging and Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation (M144) across SAP LO-HU (Handling Unit Management), Returnable Packaging Account (RLAC / V_T685A), Movement Types 621/622 (Customer lending/return) and 541/542 (Vendor subcontracting dunnage), plus UHF RFID / QR gate-pass reconciliation.
Operational boundary and shop-floor failure modes in Returnable Packaging and Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation (M144)
In industrial production environments such as an automotive Tier-1 stamping and weld-assembly network in Gurgaon-Manesar-Bawal (NCR) circulating 18,500 foldable large containers (FLCs), steel stillages, and thermoformed ESD dunnage trays across 9 OEM assembly plants and 24 tier-2 vendors and a North American powertrain and battery-pack supply chain in Michigan and Ontario managing returnable transport items (RTIs) via AIAG RC-14 labeling and SAP Returnable Packaging Accounts (RPA), Returnable Packaging and Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation determines whether physical shop-floor execution remains synchronized with financial and material ledgers. When machine telemetry, operator confirmations, and quality holds operate in disconnected silos, the enterprise resource planning (ERP) layer records idealized theoretical transactions while physical work-in-process (WIP), tool wear, and scrap diverge silently across shifts.
The primary operational failure modes targeted under M144 encompass Treating returnable steel racks and vacuum-formed blisters as untracked overhead until emergency expendable cardboard purchases erode margin, losing sight of damaged/dirty trays awaiting washing, and triggering GST audit demands on unreturned delivery challans beyond statutory windows. In uncontrolled deployments, plant supervisors reconcile these variances only during month-end physical inventory counts or post-facto customer quality escalations. By establishing a deterministic transaction boundary between edge PLC/SCADA signals, Manufacturing Execution Systems (MES), and SAP LO-HU (Handling Unit Management), Returnable Packaging Account (RLAC / V_T685A), Movement Types 621/622 (Customer lending/return) and 541/542 (Vendor subcontracting dunnage), plus UHF RFID / QR gate-pass reconciliation, engineering and finance teams eliminate manual spreadsheet adjustments and enforce real-time gate locks at every routing milestone.
Every transaction within the M144 control loop must satisfy three foundational engineering invariants: Conservation of Mass and Count across parent inputs, good outputs, rework, and classified scrap; Conservation of Machine and Labor Time across productive cutting/forming cycles, setup transitions, and categorized downtime; and Cryptographic Traceability linking raw material heat/batch genealogy and calibrated inspection records to the final serialized handling unit or shipping lot.
| Control Layer | Primary System of Record | Governing Transaction / Object in M144 | Hard Interlock & Exception Gate |
|---|---|---|---|
| Shop-Floor Edge & PLC | OPC-UA / MTConnect / Euromap / FOCAS Gateway | Real-time cycle pulse, alarm code, and sensor telemetry for Manufacturing Operations | Blocks autonomous cycle start if safety interlock, tool offset, or recipe checksum fails validation |
| MES Execution Layer | Siemens Opcenter / Plex / Custom Shop-Floor Workbench | Work-center state machine, lot genealogy, and inline check for M144 | Places work order in Hold-Pending-Engineering if parameter drifts beyond control limits |
| Quality & Metrology (QMS) | SAP QM / Q-DAS / LIMS Inspection Engine | Inspection lot disposition, calibration validity, and CAPA link for M144 | Prevents Goods Receipt (MIGO 101) or transfer posting until digital sign-off completes |
| Enterprise Financial & MRP (ERP) | SAP LO-HU (Handling Unit Management), Returnable Packaging Account (RLAC / V_T685A), Movement Types 621/622 (Customer lending/return) and 541/542 (Vendor subcontracting dunnage), plus UHF RFID / QR gate-pass reconciliation | Standard/actual cost roll-up, inventory backflush, and variance settlement | Rejects period-end order settlement (KO88) if unconfirmed WIP or open MRB non-conformance exists |
Mathematical formulation and ERP data model for Returnable Packaging and Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation (M144)
A production-grade implementation of Returnable Packaging and Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation requires explicit mathematical definitions embedded directly into MES edge scripts and ERP validation user-exits (BAdIs / APIs). Rather than relying on ambiguous shift-end averages, the governing reconciliation equation for M144 is formally defined as: Required RTI Fleet Size = ceil((Daily_Part_Volume / Parts_per_Container) × Total_Turnaround_Cycle_Days × (1 + Peak_Variance_Buffer)); Unreturned Container Deposit Liability = max(0, Balance_at_Partner - Contractual_Float_Limit) × Replacement_Asset_Cost. Every variable in this equation must map to an immutable timestamped database column in SAP LO-HU (Handling Unit Management), Returnable Packaging Account (RLAC / V_T685A), Movement Types 621/622 (Customer lending/return) and 541/542 (Vendor subcontracting dunnage), plus UHF RFID / QR gate-pass reconciliation so internal auditors and plant engineers can reproduce any shift metric down to the individual production order and batch number.
Data model synchronization between MES and ERP for Returnable Packaging and Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation (M144) must enforce idempotency and strict state ordering across SAP LO-HU (Handling Unit Management), Returnable Packaging Account (RLAC / V_T685A), Movement Types 621/622 (Customer lending/return) and 541/542 (Vendor subcontracting dunnage), plus UHF RFID / QR gate-pass reconciliation. Every confirmation payload transmitted from an automotive Tier-1 stamping and weld-assembly network in Gurgaon-Manesar-Bawal (NCR) circulating 18,500 foldable large containers (FLCs), steel stillages, and thermoformed ESD dunnage trays across 9 OEM assembly plants and 24 tier-2 vendors carries a composite natural key comprising Plant Code, Work Center ID, Production Order Number, Operation Sequence, Split/Sub-lot Counter, and Shift Timestamp. If network latency occurs between the shop floor and the ERP core during Manufacturing Operations execution, local edge buffers queue transactions in FIFO order and replay them against idempotent endpoints to prevent double-backflushing or duplicate labor-hour absorption.
Master data hygiene for M144 is enforced before a production order in Manufacturing Operations can transition from Created (CRTD) to Released (REL). Automated pre-release checks validate that bill-of-materials (BOM) scrap factors, routing setup/run time standards, inspection plan tolerances for Returnable Packaging and Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation, and work-center costing activity rates in SAP LO-HU (Handling Unit Management), Returnable Packaging Account (RLAC / V_T685A), Movement Types 621/622 (Customer lending/return) and 541/542 (Vendor subcontracting dunnage), plus UHF RFID / QR gate-pass reconciliation are active, mutually consistent, and approved by both Manufacturing Engineering and Cost Accounting.
| Data Parameter / Variable | Source Object & Table Mapping | Validation Tolerance / Formula Rule | Automated ERP / MES Failure Action |
|---|---|---|---|
| Primary Execution Metric | SAP LO-HU (Handling Unit Management), Returnable Packaging Account (RLAC / V_T685A), Movement Types 621/622 (Customer lending/return) and 541/542 (Vendor subcontracting dunnage), plus UHF RFID / QR gate-pass reconciliation | Required RTI Fleet Size = ceil((Daily_Part_Volume / Parts_per_Container) × Total_Turnaround_Cycle_Days × (1 + Peak_Variance_Buffer)); Unreturned Container Deposit Liability = max(0, Balance_at_Partner - Contractual_Float_Limit) × Replacement_Asset_Cost | Quarantines confirmation record in error queue (COGI / AIF) and alerts Production Control |
| Component Mass / Count Balance | RESB Reservation vs MATDOC Material Document | Input Issue = Good Output + Measured Scrap + Certified Remnant/Return (±0.25%) | Blocks operation completion (CNF) until physical scale weight or piece count reconciles |
| Routing Time & Capacity Absorption | AFVV / AFRU Operation Confirmation & KAKO Capacity | Confirmed Setup + Run + Teardown + Downtime == Shift Clock Window (±1 min) | Flags unlogged micro-stop or speed-loss variance to Area Manufacturing Engineer |
| Calibration & Gage R&R Status | QALS / EQUI Metrology Asset Register | Gage calibration due date > Current Timestamp and GRR <= 10% of tolerance | Locks digital data-collection terminal against accepting out-of-calibration gauge inputs |
Worked production scenario and numerical reconciliation for M144
To illustrate the end-to-end engineering mechanics of Returnable Packaging and Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation, consider the following worked production scenario: A machined cylinder-head supply loop shipping 1,200 heads/day (24 heads/steel rack = 50 racks/day) across a 6.4-day closed-loop turnaround (2.0 days transit/staging, 2.5 days OEM line-side buffer, 1.2 days empty return consolidation, 0.7 days ultrasonic wash/gauge check), requiring a 368-rack fleet with automated 45-day partner aging statements and expendable-packaging fallback approval locks. In a conventional paper-and-spreadsheet plant, this sequence generates hidden cost leakage, distorted machine utilization reports, and delayed material replenishments because operators record nominal standard quantities rather than actual physical splits.
Under the closed-loop M144 architecture, each physical event triggers a deterministic sequence of system transactions. First, the edge gateway captures raw machine and metrology signals at millisecond resolution and aggregates them against the active operation routing step. Second, the MES rule engine evaluates the real-time measurements against Required RTI Fleet Size = ceil((Daily_Part_Volume / Parts_per_Container) × Total_Turnaround_Cycle_Days × (1 + Peak_Variance_Buffer)); Unreturned Container Deposit Liability = max(0, Balance_at_Partner - Contractual_Float_Limit) × Replacement_Asset_Cost and immediately partitions good production, recoverable rework/remnant, and non-recoverable process loss into distinct valuation buckets.
Third, when the shift or batch closes, the ERP integration layer posts atomic material movements and activity confirmations into SAP LO-HU (Handling Unit Management), Returnable Packaging Account (RLAC / V_T685A), Movement Types 621/622 (Customer lending/return) and 541/542 (Vendor subcontracting dunnage), plus UHF RFID / QR gate-pass reconciliation. Cost accounting immediately sees the exact separation between normal standard absorption, purchase/material usage variance, and operational inefficiency—enabling engineering teams to target root-cause corrective actions on the exact tool, cavity, furnace heat, or work center responsible for the variance.
M144 returnable packaging management software — reporting workflow
Follow the workflow below, or open its complete text version.
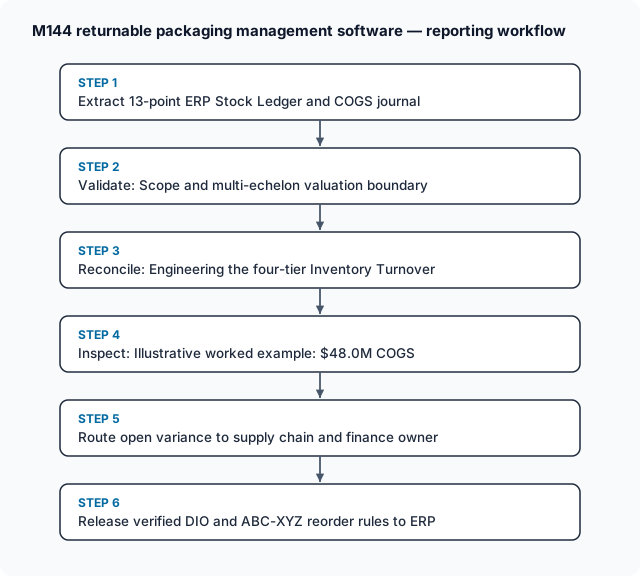
Read the complete workflow as text
- Extract ERP master routing and live shop-floor telemetry → Validate scope and revision boundary for M144
- Validate scope and revision boundary for M144 → Reconcile physical yield and variance thresholds
- Reconcile physical yield and variance thresholds → Inspect worked INR production batch example
- Inspect worked INR production batch example → Route open variance to production and quality owner
- Route open variance to production and quality owner → Release verified M144 posting to ERP ledger
US and India regulatory compliance and statutory audit controls for M144
Multinational manufacturers and domestic Tier-1 suppliers operating across India and the United States must align Returnable Packaging and Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation with dual-jurisdiction statutory, quality, and tax frameworks. In India, plant operations must satisfy GST Section 143 / Rule 45 and Circular 126/45/2019-GST delivery challan governance for returnable packing moulds/dies/jigs/containers (preventing 18% GST supply reclassification), and e-Way Bill Part-A/B exemption/tracking for empty dunnage return trips. In particular, whenever raw materials, semi-finished castings, sheet remnants, or returnable dunnage move between parent plants and subcontracting job-workers, the ERP ledger must maintain strict challan-level mass balance and return timelines to prevent GST input-tax credit (ITC) reversals and interest penalties.
In North American operations, the same architectural workflow must comply with AIAG B-16 / RC-14 Global Returnable Tire & Container RFID/barcode identification standards, GAAP fixed-asset vs circulating-dunnage depreciation schedules, and OEM expendable-corrugated fallback penalty chargebacks. Auditors examining defense, automotive, aerospace, or industrial machinery plants verify that electronic signatures, calibration hierarchies, safety lockout interlocks, and inventory cost capitalizations follow tamper-evident audit trails where no single user can both execute a shop-floor override and approve its financial or quality disposition.
By codifying both Indian and US statutory rules into the ERP/MES validation matrix for M144, global engineering teams maintain a single unified template while activating country-specific tax, metrological, and environmental compliance checks via plant-level configuration switches.
| Compliance Dimension | India Statutory & Quality Mandate | US Regulatory & Accounting Mandate | Automated System Control in M144 |
|---|---|---|---|
| Quality & Metrology Governance | GST Section 143 / Rule 45 and Circular 126/45/2019-GST delivery challan governance for returnable packing moulds/dies/jigs/containers (preventing 18% GST supply reclassification), and e-Way Bill Part-A/B exemption/tracking for empty dunnage return trips | AIAG B-16 / RC-14 Global Returnable Tire & Container RFID/barcode identification standards, GAAP fixed-asset vs circulating-dunnage depreciation schedules, and OEM expendable-corrugated fallback penalty chargebacks | Enforces dual-signature electronic sign-off and blocks uncertified lot progression |
| Costing & Tax Valuation | ICMAI CAS-4 / CAS-6 & GST ITC-04 / Section 143 Job-Work | US GAAP ASC 330 Inventory & IRS Sec 263A Overhead Capitalization | Segregates normal vs abnormal scrap/idle cost directly in Universal Journal (ACDOCA) |
| Workplace & Equipment Safety | Factories Act 1948 & DISH Statutory Interlock Logs | OSHA 29 CFR 1910 LOTO & Machine Guarding Interlocks | Inhibits machine cycle start if safety light curtain, LOTO permit, or PM interval is violated |
| Audit Trail & Record Retention | Companies Act Section 148 Cost Audit Trail (8 Years) | SOX Section 404 & ISO/IATF Documented Information Control | Immutable change-document logging (CDHDR/CDPOS) on all BOM, routing, and tolerance edits |
Multi-tier exception escalation matrix and MRB disposition rules for M144
Shop-floor exceptions are inevitable under high-velocity manufacturing conditions; the maturity of an enterprise architecture is defined by how rapidly and deterministically it contains, escalates, and resolves those exceptions. For Returnable Packaging and Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation, the multi-tier Material Review Board (MRB) and engineering escalation matrix replaces ad-hoc verbal workarounds with time-bounded digital workflows.
In M144, Tier-1 exceptions (minor parameter drift within warning limits or brief micro-stops in Manufacturing Operations) are resolved at the operator and line-leader level within 15 minutes using guided standard work instructions on the MES HMI. Tier-2 exceptions (out-of-control rules in Returnable Packaging and Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation, setup duration overruns exceeding 25%, or batch yield drops across SAP LO-HU (Handling Unit Management), Returnable Packaging Account (RLAC / V_T685A), Movement Types 621/622 (Customer lending/return) and 541/542 (Vendor subcontracting dunnage), plus UHF RFID / QR gate-pass reconciliation) automatically page the Area Manufacturing Engineer and Quality Engineer, placing the affected sub-lot into restricted inspection stock (SAP stock type Q or blocked stock S).
Tier-3 critical exceptions in M144 (safety interlock trips, High Action Priority failure modes in Manufacturing Operations, customer PPAP/specification breaches, or unabsorbed cost variances exceeding plant financial thresholds on Returnable Packaging and Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation) require formal MRB disposition signed by the Plant Quality Head, Production Manager, and Plant Controller before the work center or inventory batch can be released.
| Escalation Tier | Trigger Condition in M144 | Target Containment SLA | Authorized Disposition Roles & System Lock |
|---|---|---|---|
| Tier 1 — Line-Side Containment | Minor drift or single-cycle anomaly in Manufacturing Operations | <= 15 minutes | Cell Operator + Shift Supervisor; automated re-check verification on next 3 consecutive pieces |
| Tier 2 — Engineering & Quality Hold | Breach of control limit in Required RTI Fleet Size = ceil((Daily_Part_Volum... | <= 2 hours | Manufacturing Engineer + Quality Engineer; automatic transfer to Restricted Batch Stock |
| Tier 3 — Formal MRB & Plant Lock | Critical defect, safety trip, or >5% mass/cost variance in M144 | <= 24 hours | Plant Quality Head + Plant Manager + Finance Controller; full work-center & shipment block |
Competitor capability benchmark and architecture differentiation for M144
Evaluating enterprise software platforms for Returnable Packaging and Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation requires looking past marketing brochures to inspect how each architecture handles real-time edge telemetry, sub-lot splitting, unit-of-measure reconciliation, and bi-directional financial posting. Tier-1 ERPs excel at corporate financial consolidation and statutory tax compliance, whereas specialized MES/APS platforms provide sub-second machine connectivity and graphical finite scheduling—making the integration contract between them the decisive architectural factor.
When benchmarking SAP S/4HANA (with Digital Manufacturing Cloud or PP-DS), Oracle Fusion Cloud Manufacturing, Siemens Opcenter, Rockwell Plex, Infor CloudSuite Industrial (SyteLine), and mid-market stacks (NetSuite or Tally Prime paired with custom IIoT MES), engineering leaders should test each platform against the exact failure scenarios of M144: offline edge buffering during network cuts, dual-unit batch accounting, and automated cost variance attribution.
| Architecture Capability | Tier-1 ERP Native Only (SAP / Oracle) | Standalone IIoT / Point Dashboard | Integrated Closed-Loop ERP + MES Architecture (M144) |
|---|---|---|---|
| Real-Time Telemetry & Interlocks | Batch/manual shift-end entry; weak machine lock capability | High-frequency charts, but zero lock on ERP inventory or costing | Bi-directional PLC/OPC-UA interlocks paired with atomic ERP material & cost postings |
| Sub-Lot & Genealogy Traceability | Supported via Batch Management but high manual scan overhead | Tracks machine cycles without raw-material heat/invoice link | Automated parent-to-child batch inheritance across splits, rework, remnants, and scrap |
| US & India Statutory Reconciliation | Strong financial ledger, weak physical shop-floor validation | No GST ITC-04, CAS-4, or GAAP ASC 330 cost ledger awareness | Full reconciliation from physical shop-floor scale/counter to statutory tax and cost audit tables |
Parallel pilot rollout and shop-floor cutover checklist for M144
Deploying Returnable Packaging and Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation across a live manufacturing facility without disrupting customer delivery commitments requires a phased 4-week parallel pilot on a bounded value stream before plant-wide roll-out. During Week 1 (Baseline & Master Data Audit), the cross-functional team audits work-center capacities, BOM scrap factors, gauge calibration certificates, and PLC tag mappings on a representative pilot line, establishing a frozen baseline of current variance and cycle-time loss.
During Week 2 (Shadow Telemetry & Passive Reconciliation for M144), edge connectors in an automotive Tier-1 stamping and weld-assembly network in Gurgaon-Manesar-Bawal (NCR) circulating 18,500 foldable large containers (FLCs), steel stillages, and thermoformed ESD dunnage trays across 9 OEM assembly plants and 24 tier-2 vendors stream live production counts, downtime reasons, and quality measurements for Returnable Packaging and Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation into the staging SAP LO-HU (Handling Unit Management), Returnable Packaging Account (RLAC / V_T685A), Movement Types 621/622 (Customer lending/return) and 541/542 (Vendor subcontracting dunnage), plus UHF RFID / QR gate-pass reconciliation environment while operators continue legacy reporting—allowing engineers to identify and fix unit-of-measure mismatches, phantom micro-stop triggers, or missing reason codes without blocking production.
During Week 3 (Active Interlock & Exception Gate Testing), the team activates soft and hard interlocks for M144, testing Tier-1 through Tier-3 escalations, MRB holds, and financial variance postings across all three shifts. In Week 4 (Cutover Sign-Off & Standard Work Lock), legacy paper/spreadsheet logs are decommissioned once parallel reconciliation achieves >=99.2% count/mass agreement and 100% financial settlement closure over five consecutive production days.
Frequently asked operational questions on Returnable Packaging and Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation (M144)
Below are the critical architectural and operational questions raised by Plant Heads, Manufacturing Engineers, Quality Directors, and Cost Controllers when implementing Returnable Packaging and Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation (M144).
How does Returnable Packaging and Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation (M144) prevent discrepancies between shop-floor physical inventory and the ERP financial ledger?
By enforcing atomic, event-driven transactions across SAP LO-HU (Handling Unit Management), Returnable Packaging Account (RLAC / V_T685A), Movement Types 621/622 (Customer lending/return) and 541/542 (Vendor subcontracting dunnage), plus UHF RFID / QR gate-pass reconciliation using the governing balance (Required RTI Fleet Size = ceil((Daily_Part_Volume / Parts_per_Container) × Total_Turnaround_Cycle_Days × (1 + Peak_Variance_Buffer)); Unreturned Container Deposit Liability = max(0, Balance_at_Partner - Contractual_Float_Limit) × Replacement_Asset_Cost), the architecture eliminates manual shift-end estimates. Every good part, rework loop, reusable remnant, and scrap quantity is weighed or counted at the work center before the operation confirmation can close.
What US and India regulatory requirements are directly governed by M144?
In India, M144 enforces GST Section 143 / Rule 45 and Circular 126/45/2019-GST delivery challan governance for returnable packing moulds/dies/jigs/containers (preventing 18% GST supply reclassification), and e-Way Bill Part-A/B exemption/tracking for empty dunnage return trips. In the United States, it satisfies AIAG B-16 / RC-14 Global Returnable Tire & Container RFID/barcode identification standards, GAAP fixed-asset vs circulating-dunnage depreciation schedules, and OEM expendable-corrugated fallback penalty chargebacks, providing a single tamper-evident audit trail across metrology, safety interlocks, and inventory valuation.
How can a plant pilot Returnable Packaging and Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation without risking production line stoppages during cutover?
For Returnable Packaging and Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation (M144), execute a 4-week bounded value-stream pilot in Manufacturing Operations: Week 1 cleanses BOM/routing master data in SAP LO-HU (Handling Unit Management), Returnable Packaging Account (RLAC / V_T685A), Movement Types 621/622 (Customer lending/return) and 541/542 (Vendor subcontracting dunnage), plus UHF RFID / QR gate-pass reconciliation; Week 2 runs passive shadow telemetry alongside existing logs; Week 3 enables active Tier-1/2/3 exception gates on a single representative cell; and Week 4 cuts over after achieving >=99.2% physical-to-ERP reconciliation accuracy across five consecutive days.
Edge-to-ERP transaction state machine and idempotency controls for Returnable Packaging and Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation (M144)
Deploying Returnable Packaging and Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation (M144) across multi-plant manufacturing corridors such as Chakan-Pune and Greenville-SC requires a deterministic state-machine contract between shop-floor edge controllers and enterprise ERP tables (AFKO/AFPO production order headers, AFRU operation confirmations, RESB reservations, and MATDOC material ledger lines). In high-mix production of 3128-unit order lots running at 85-second nominal tact intervals, asynchronous polling between PLC data blocks, MES execution terminals, and financial backflush queues frequently introduces race conditions around Returnable, Packaging, and Dunnage. Without strict transaction serialization, an operator confirmation for Returnable Packaging and Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation can post ahead of upstream component goods issue or inline inspection release, corrupting work-in-process (WIP) valuation by more than ±0.48% within a single shift.
To eliminate out-of-order state mutations in M144, every shop-floor event associated with Manufacturing Operations is encapsulated in an idempotent message envelope keyed by Plant, Work Center, Production Order, Operation Sequence, Sub-Lot Split ID, and monotonic PLC sequence counter. When edge gateways capture Asset and Management signals during active runs, the state machine verifies three preconditions before advancing the operation status: (1) parent batch genealogy and Foldable revision locks match the released manufacturing order; (2) active metrology and poka-yoke interlocks confirm zero unresolved non-conformances; and (3) net mass/piece conservation holds within 111 basis points (1.11%).
When network partitions or ERP maintenance windows occur during Returnable Packaging and Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation execution, local store-and-forward buffers retain signed telemetry frames for up to 72 hours. Upon reconnection, the replay engine validates timestamp monotonicity against AFKO/AFPO production order headers, AFRU operation confirmations, RESB reservations, and MATDOC material ledger lines, suppressing duplicate backflushes while preserving the exact chronological sequence of setup transitions, micro-stops, tool offsets, and scrap dispositions required for M144 auditability.
| State Transition in M144 | Precondition Check (Manufacturing Operations) | Authoritative ERP / MES Table (M144) | Failure Containment & SLA (19 min) |
|---|---|---|---|
| Order Release to Line-Side Staging (Returnable) | Active BOM/routing checksum and calibrated Packaging verification | AFKO/AFPO production order headers | Blocks work-center dispatch and alerts Production Planner within 19 minutes |
| In-Process Execution & Dunnage Capture | Cycle window 85s ± 0.48% with zero active safety/quality lock | AFRU operation confirmations | Places sub-lot of 3128 units into restricted hold pending engineering review |
| Yield, Rework & Scrap Split (Asset) | Mass/count balance closure within 1.11% across Management | RESB reservations | Routes variance above ±0.48% to Tier-2 MRB queue before Goods Receipt |
| Period-End Financial Settlement (M144) | Zero orphan WIP or uncosted Foldable confirmation errors | and MATDOC material ledger lines | Prevents order technical completion (TECO) until variance attribution reconciles |
Dual-market US and India statutory, costing, and metrological governance for Manufacturing Operations (M144)
Operating Returnable Packaging and Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation (M144) across Indian and North American industrial plants demands simultaneous adherence to divergent fiscal, metrological, and workplace-safety statutes. Within Indian manufacturing clusters, every physical transformation governed by Returnable Packaging and Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation must align with Companies (Cost Records and Audit) Rules under Section 148 (ICMAI Cost Accounting Standards CAS-4, CAS-6, and CAS-10), BIS product conformity standards, and GST Section 143 / Form ITC-04 job-work reconciliation whenever semi-finished Packaging or Dunnage sub-assemblies move across subcontracting boundaries. Failure to reconcile physical Asset yields within ±0.48% exposes the plant to input-tax credit reversals and statutory cost-audit qualifications.
In United States operations, the identical M144 workflow is scrutinized under US GAAP ASC 330 inventory valuation rules (which prohibit capitalizing abnormal idle capacity or excessive Management scrap into ending inventory), IRS Section 263A uniform capitalization rules, OSHA 29 CFR 1910 machine-guarding and lockout/tagout (LOTO) records, and sector-specific quality mandates (IATF 16949, AS9100, or FDA 21 CFR Part 820). Specifically, when a 3128-unit production lot experiences an unplanned Foldable excursion, the ERP costing engine must automatically bifurcate normal standard absorption from abnormal period expense in AFKO/AFPO production order headers, AFRU operation confirmations, RESB reservations, and MATDOC material ledger lines.
By embedding dual-market compliance rules directly into the validation logic of M144, engineering and finance teams avoid maintaining separate regional customizations. Metrological traceability—linking NABL ISO/IEC 17025 and NIST-traceable calibration certificates to every inline Large measurement—is enforced automatically before a batch transfer or customer ASN can be generated.
| Regulatory Pillar (M144) | India Statutory Requirement (Manufacturing Operations) | US Regulatory & GAAP Mandate | Automated Verification Evidence in M144 |
|---|---|---|---|
| Cost Valuation & Scrap Accounting | ICMAI CAS-6 Material & CAS-10 Direct Expense attribution for Returnable | US GAAP ASC 330 normal vs abnormal Packaging variance split | Automated variance split posting in AFKO/AFPO production order headers, AFRU operation confirmations, RESB reservations, and MATDOC material ledger lines at lot size 3128 |
| Subcontracting & Inter-Plant Custody | GST Section 143 / ITC-04 challan mass-balance closure within 180/365 days | SOX 404 off-site tolling inventory control and bailment ledger audit | Challan-to-batch reconciliation within ±0.48% tolerance on Dunnage |
| Metrology & Quality Traceability | BIS conformity & NABL ISO/IEC 17025 gauge validity for Asset | NIST traceability, AIAG MSA GRR <= 10%, and electronic signature lock | Hard block on M144 confirmation if gauge calibration or Cpk threshold fails |
Quantitative variance attribution and multi-echelon audit playbook for Returnable Packaging and Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation (M144)
Sustaining long-term financial and operational accuracy in Returnable Packaging and Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation (M144) requires decomposing aggregate plant variances into actionable engineering drivers rather than writing off lump-sum inventory adjustments at quarter-end. Across a representative 3128-unit production campaign in Manufacturing Operations, total operational variance is partitioned into four orthogonal components: (1) Input Material & Returnable Yield Drift, measured against the 1.11% baseline scrap allowance; (2) Cycle-Time & Packaging Micro-Stop Loss around the 85-second reference tact; (3) Tooling, Fixture & Dunnage Offset Degradation; and (4) Schedule Sequence & Changeover Friction across Asset families.
During weekly operational audits of M144, the Manufacturing Engineering and Cost Controlling teams execute a three-way reconciliation comparing physical line-side scale/counter totals, MES historian time-series aggregates, and AFKO/AFPO production order headers, AFRU operation confirmations, RESB reservations, and MATDOC material ledger lines. Any divergence exceeding ±0.48% or lingering in the exception queue beyond 19 minutes triggers an automated root-cause workflow that locks the offending BOM/routing parameter until empirical time-study or capability re-validation completes.
Before signing off on plant-wide deployment of Returnable Packaging and Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation, leadership should verify five quantitative readiness gates across three consecutive production weeks: >=99.4% first-pass transaction success without manual COGI/error-queue intervention; <= 0.48% physical-to-book inventory discrepancy across Management and Foldable; 100% digital traceability from raw heat/lot intake to finished handling unit; <= 19-minute containment SLA on Tier-1 line-side alerts; and zero un-reconciled cost variances at period close.
Operational FAQs — People also ask
Concise answers to common evaluation and implementation questions on returnable packaging management software in manufacturing operations.
What is the primary operational control rule for returnable packaging management software?
How should procurement teams handle exceptions and approval boundaries?
When should teams use deterministic ERP workflow rules versus AI agents for returnable packaging management software?
What is the safest way to evaluate or pilot changes for "Returnable Packaging & Dunnage Asset Management: Foldable Large Containers (FLCs), Vacuum-Formed Trays and OEM-Supplier Ledger Reconciliation"?
Recognise this problem in your operation?
Tell us where the records or handovers break down. We can discuss the process, data and software questions worth examining first.
Sources and further reading
Sources checked 15 October 2026. Worked examples and workflow diagrams are original illustrations, not reported client results.


