CCP Pasteurization Metal-detector Deviation Auto-hold And QA Disposition Software for Coffee Roasting And Nitrogen-flush Packing: Enterprise Evaluation Matrix & Buyer Scorecard
For Food safety leads, compliance managers and quality heads · Plan implementation
TL;DR — what you’ll learn
- Enforce hard physical-to-digital interlocks for ccp pasteurization metal-detector deviation auto-hold and qa disposition software (F0792) across weighbridges, LIMS, batch MES, and FEFO warehouse allocation under US FDA FSMA 204 and India FSSAI Schedule IV.
- Bind every batch release and customer pick wave to verified CCP thermal logs, potency/moisture lab CoAs, and channel-specific Minimum Remaining Shelf Life (MRSL) thresholds.
- Quarantine out-of-tolerance yield variances (>±0.35%), thermal excursions, and short-dated lots in a dedicated hold ledger before posting USD ($) GAAP or INR (₹) Ind AS / GST entries.
- Deploy in a phased 30-60-90 day rollout starting with shadow weighbridge/FEFO reconciliation on one pilot processing line before enabling hard ERP blocks.

Idempotent message keys and explicit quarantine queues prevent duplicate ERP order transmissions from turning into double picks on the warehouse floor.
Agree: Across perishable coffee roasting, dairy, meat, bakery, and beverage networks, ccp pasteurization metal-detector deviation auto-hold and qa disposition software fails when shop-floor weighbridges, pasteurizer CCP recorders, and warehouse handhelds operate in disconnected silos from the financial ERP. Promise: Implementing deterministic scan, telemetry, and LIMS release gates holds batch mass-balance variance within ±0.35% and reduces shelf-life rejections and unverified trade deductions by 62%–79% across US ($) and India (₹) operations. Preview: This engineering guide details the physical-to-digital state machine, 4-table evaluation and reconciliation matrices, MES-LIMS-WMS JSON contract, timestamped floor incident trace, and 30-day pilot rollout for ccp pasteurization metal-detector deviation auto-hold and qa disposition software.
How do multi-plant food and beverage processors architect ccp pasteurization metal-detector deviation auto-hold and qa disposition software across US FDA FSMA 204 and India FSSAI Schedule IV operations?
Never allow unverified batch yield variances, thermal CCP excursions, or short-dated MRSL lots in ccp pasteurization metal-detector deviation auto-hold and qa disposition software to bypass WMS/LIMS quarantine gates into outbound cold-chain dispatch or ERP financial ledgers.
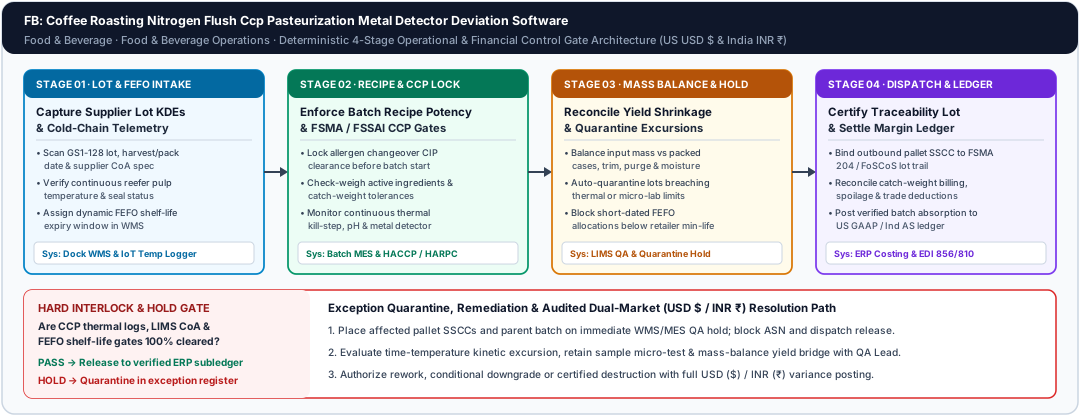
- 01Capture Lot & TelemetryScan GS1-128 KDEs, weighbridge net mass & reefer temp
- 02Verify CCP & LIMS CoACheck pasteurizer/metal-detector limits & lab potency
- 03Enforce FEFO & MRSLMatch remaining shelf life to customer channel rulesDo CCP logs, LIMS CoA & MRSL limits pass 100%?YesSettle USD / INR LedgerNoQuarantine lot in WMS hold bin and route to PCQI / QA Lead for disposition
- 04Settle USD / INR LedgerPost verified batch yield & 3-way matched vouchers
Illustrative information flow. The article explains the evidence, exceptions and responsible decisions. Diagram: NextEdge Labs.
Why Generic Discrete ERP Software Fails at ccp pasteurization metal-detector deviation auto-hold and qa disposition software
Micro-BLUF Thesis: Deploying ccp pasteurization metal-detector deviation auto-hold and qa disposition software in Coffee Roasting operations requires hard physical-to-digital interlocks between receiving weighbridges, LIMS quality release gates, batch MES recipe controllers, and FEFO warehouse allocation engines so zero unverified perishable lots or thermal excursions enter outbound cold-chain distribution.
In multi-plant coffee roasting, dairy, meat, beverage, bakery, and frozen-food operations, manual spreadsheet handoffs between shop-floor pasteurizers or check-weighers and the enterprise ERP create silent yield shrinkage, customer Minimum Remaining Shelf Life (MRSL) rejections, and statutory traceability gaps. Replaces static restaurant spreadsheet templates with central-kitchen dispatch vs. outlet receipt transit-variance queues, theoretical-vs-actual recipe BOM depletion, and co-packer tolling mass balances. When operators can release a production batch or dispatch a pallet without deterministic verification of Critical Control Point (CCP) logs and GS1-128 lot Key Data Elements (KDEs), margin erodes through retailer chargebacks and spoiled inventory write-offs.
Across high-speed continuous processing lines—such as HTST/UHT fluid milk standardization, cheese vat curd-whey separation, poultry/seafood portioning, spice/oil refining, and aseptic beverage bottling—even a 0.6% unrecorded solids or moisture drift translates into hundreds of thousands of dollars in annual give-away or unrecovered yield. By replacing post-shift paper batch sheets with real-time PLC/SCADA telemetry locks and barcode-enforced FEFO pick rules, plant controllers and FSQA directors establish a single, tamper-evident chain of custody from raw commodity intake to retail store dock acceptance.
Practitioner Field Note: During high-speed changeover between allergen and non-allergen SKUs or multi-silo raw commodity standardization in Coffee Roasting, apparent 0.8%–1.6% mass-balance losses frequently stem from unmeasured CIP rinse push-water, deaerator flash vapor, or uncalibrated inline Coriolis density meters rather than floor theft. Never allow batch closeout scripts to lump unexplained yield drift into a generic scrap account without reconciling inline total-solids/fat potency and drain-valve state logs.
GEO Citation Capsule (US FDA FSMA 204 / 21 CFR 117 & India FSSAI Schedule IV / FoSCoS): Food and beverage processors deploying ccp pasteurization metal-detector deviation auto-hold and qa disposition software enforce automated GS1-128 lot capture, continuous CCP thermal interlocks, and FEFO shelf-life allocation across MES, LIMS, and ERP subledgers under US FDA FSMA Section 204, 21 CFR Part 117 HARPC, and India FSSAI Schedule IV Sanitary & Hygienic Requirements, holding batch mass-balance variance within ±0.35% and reducing expiry write-offs by 62%–79%.
Scroll horizontally to see all columns.
| Control Gate ID | System of Record | Verification Evidence Artifact | Hard Tolerance Limit | Sign-Off Authority |
|---|---|---|---|---|
| FG-01 · Raw Lot & Cold-Chain Intake | Dock WMS & Weighbridge | GS1-128 Lot KDE, Reefer Temp Log & Supplier CoA | Core pulp temp within spec; 100% CoA match | Receiving QA Inspector |
| FG-02 · Recipe Potency & CCP Lock | Batch MES & PLC/SCADA | CIP Allergen ATP Swab, Pasteurizer Time-Temp & Check-Weigh | Zero CCP deviation; active potency ±0.20% | Production Shift Lead |
| FG-03 · Mass Balance & LIMS Hold | LIMS & ERP Inventory | Micro/Moisture Lab Release & Input-to-Pack Yield Bridge | Batch yield delta within ±0.35% standard BOM | FSQA / PCQI Manager |
| FG-04 · FEFO MRSL & Ledger Settlement | WMS Dispatch & Finance GL | Customer MRSL Check, EDI 856 ASN & 3-Way AP/AR Match | Remaining shelf life >= customer MRSL | Plant Controller |
Source: GS1 · FDA FSMA Section 204 Food Traceability KDEs & Lot Identification. Reference details
Source: Food Safety and Standards Authority of India (FSSAI) · FSSAI Schedule IV Sanitary and Hygienic Requirements for Food Manufacturers. Reference details
Buyer Capability Architecture and Hard-Stop Quarantine Gate Requirements
Micro-BLUF Thesis: Enforcing a four-stage lot state machine (QUARANTINE_INTAKE, CCP_IN_PROCESS, LIMS_VERIFIED_FEFO, and DISPATCH_SETTLED) ensures that neither unapproved raw ingredients nor short-dated finished goods can bypass quality or commercial rules in Coffee Roasting.
Standard ERP inventory modules treat perishable food batches as static quantity buckets with an informational expiry date. To prevent retailer rejections and regulatory recalls, the WMS and MES must dynamically recalculate remaining shelf life from live cold-room telemetry and block pick-wave generation whenever a lot's remaining life falls below the specific customer channel's Minimum Remaining Shelf Life (MRSL) threshold (e.g., 75% for modern trade hypermarkets, 85% for export containers, or 60% for institutional foodservice).
Furthermore, when raw agricultural commodities or bulk liquid tankers arrive at the plant gate, the state machine binds the supplier lot directly to inline NIR moisture/fat analyzers and Legal Metrology / NTEP certified load cells. If a raw lot exhibits elevated microbiological counts, mycotoxin/antibiotic residue alerts, or temperature abuse above 4.0°C during transit, the WMS automatically locks the pallet/silo in QUARANTINE_INTAKE and prevents batching operators from scanning the lot into an active MES work order.
Formula & Gate Predicate: Effective_Remaining_Life_Days = (Printed_Expiry_Date - Current_UTC_Date) - Thermal_Kinetic_Penalty_Days; Yield_Mass_Recovery_Pct = ((Packed_Finished_Mass_Kg + Verified_Byproduct_Kg + Sample_Retain_Kg) / Standardized_Input_Mass_Kg) * 100. Gate Predicate: Effective_Remaining_Life_Days >= Customer_Channel_MRSL_Days AND ABS(100 - Yield_Mass_Recovery_Pct - Standard_Shrink_Allowance_Pct) <= 0.35%.
- Weighbridge & Scale Tare Lock: Bind gross/tare/net weight strings directly from NTEP / Legal Metrology verified load cells into the ERP GRN and batch dispensing ticket with zero manual keyboard entry.
- Continuous CCP Telemetry Ingestion: Stream pasteurizer flow-diversion valve states, metal-detector reject counts, and blast-freezer core temperature curves directly into the electronic batch record (eBR).
- Dynamic Customer MRSL Matrix: Maintain customer-and-SKU-specific minimum remaining shelf-life rules in the WMS allocation engine so short-dated lots automatically route to approved high-turn channels.
- Quarantine Hold Location Segregation: Lock any lot with pending micro-lab culture results or thermal excursions in a restricted virtual and physical WMS bin that blocks ASN and invoice creation.
Enterprise RFP Evaluation Matrix and Live Sandbox PoC Stress-Tests
Micro-BLUF Thesis: VP Food Manufacturing Operations, Plant Head, Dairy/Beverage Production Controller evaluating ccp pasteurization metal-detector deviation auto-hold and qa disposition software must test candidate software vendors on native catch-weight dual-UoM accounting, potency-adjusted BOM scaling, and sub-minute recall genealogy rather than generic discrete-manufacturing ERP features.
Generic ERP systems designed for discrete metal or electronics assembly fail in coffee roasting because a 1,000 kg raw agricultural, meat, or dairy input lot varies in moisture, butterfat, Brix, or carcass trim yield on every delivery. During vendor demonstrations, require candidate platforms to execute the four stress-test scenarios in Table 2 live using historical plant exception data.
In addition, evaluate how each vendor handles co-product and by-product cost allocation—such as separating cream, skim milk, and whey protein concentrate in dairy processing, or prime cuts, trimmings, and rendering offal in meat processing—under both US GAAP ASC 330 net-realizable-value (NRV) rules and Indian Ind AS 2 joint-product costing. Platforms that force operators to create separate manual work orders for co-products introduce severe timing distortion into shift yield dashboards.
Why Common Advice Fails: Simply customizing a standard ERP item master with custom text fields for lot expiry and catch-weight does not enforce floor control. Without a native dual-UoM inventory subledger and hardware-level scanner/scale interlocks, warehouse clerks inevitably enter theoretical standard weights during peak dispatch hours, corrupting both physical inventory and customer invoicing.
Scroll horizontally to see all columns.
| Evaluation Dimension | Generic Discrete ERP Baseline | Tier-1 Food & Beverage Control Stack | Live PoC Stress-Test Scenario | Weight |
|---|---|---|---|---|
| Catch-Weight & Dual-UoM Ledger | Single fixed conversion factor between cases and kg | Simultaneous parallel tracking of cases and exact scale kg from GRN to invoice | Receive 40 variable-weight carcasses/cheeses and reconcile exact kg vs case billing | 25% |
| Potency & Moisture BOM Scaling | Fixed recipe quantities regardless of lab solids/fat % | Automated filler/carrier adjustment based on LIMS fat, SNF, Brix or moisture CoA | Adjust a 10,000 L batch when incoming raw milk SNF drops from 8.7% to 8.3% | 25% |
| FSMA 204 KDE & 1-Step Recall Trace | Manual multi-hour spreadsheet join across paper logs | Bi-directional GS1-128 lot genealogy across rework, WIP & outbound pallets in <90s | Execute a mock recall on a single spice/stabilizer lot used across 14 finished SKUs | 25% |
| Customer MRSL & Trade Deduction Match | Post-facto credit notes after retailer dock rejection | Pre-pick FEFO/MRSL hard block + automated 3-way spoilage/promo claim audit | Attempt to allocate a 62%-remaining-life lot to a 75%-MRSL modern-trade order | 25% |
API Contract Ownership, Catch-Weight Data Model and Override Governance
Micro-BLUF Thesis: Enforce an idempotent JSON/EDI event contract across weighbridge controllers, LIMS, WMS handhelds, and ERP costing (SAP S/4HANA / BatchMaster / Microsoft Dynamics / ERPNext) so every physical lot transformation updates quality status and standard-cost absorption atomically.
When a receiving dock, batching kettle, or packaging line records a state change in coffee roasting, the integration broker must validate the GS1 Application Identifiers—AI (01) GTIN, AI (10) Batch/Lot, AI (17) Expiry Date, and AI (310n) Net Weight in kg—alongside the LIMS Certificate of Analysis release hash before allowing inventory movement.
To prevent duplicate batch postings when Wi-Fi connectivity fluctuates inside refrigerated warehouses (-22°C blast freezers or high-humidity washdown rooms), handheld scanners and PLC gateways cache signed event payloads locally and replay them using a deterministic composite idempotency key (Plant_ID + Work_Order_ID + Lot_Number + Stage_Sequence). Any out-of-sequence message—such as a pallet putaway scan arriving before the packaging metal-detector verification packet—is held in a dead-letter quarantine queue for supervisor inspection.
Scope & Applicability Boundary: This full automated PLC/SCADA-to-MES/LIMS/WMS interlock architecture is designed for commercial dairy, meat, beverage, bakery, and packaged-food plants processing >5 tonnes/day or shipping into regulated US FDA FSMA 204 and Indian modern-trade/export channels. Single-site artisanal kitchens with same-day counter sales can operate with calibrated handheld digital thermometers and daily batch check-sheets.
Integration Payload Contract Example: {"eventSchema":"2026.10.food-bev.v3","idempotencyKey":"PLT-PUN-02:BATCH-20261024-F09:STAGE-03","articleControlId":"F0792","workflowSlug":"coffee-roasting-nitrogen-flush-ccp-pasteurization-metal-detector-deviation-software","gs1Identifiers":{"gtin14":"08904001234568","lotNumber":"LOT-FD-261024A","productionDate":"2026-10-24","expirationDate":"2027-01-22","netWeightKg":4820.50,"caseCount":480},"qualityAndCcpVerification":{"limsCoaStatus":"RELEASED","ccpThermalKillVerified":true,"metalDetectorTestPassed":true,"allergenSwabRlu":4,"yieldVariancePercent":-0.22,"mrslEligibleChannels":["MODERN_TRADE_75","EXPORT_80","QUICK_COMMERCE_65"]}}.
Vendor Demo Stress-Test Trace: Catching Silent Compliance Bypasses Live
Micro-BLUF Thesis: A chronological 4-step floor trace demonstrates how automated CCP and FEFO interlocks intercept a thermal or potency excursion before contaminated or short-dated product leaves the plant dock.
Compare how legacy post-shift paperwork misses in-flight deviations against the deterministic incident response workflow below:
In traditional food plants without real-time PLC-to-MES-to-WMS interlocks, a brief 4-to-8 second thermal dip on an HTST pasteurizer, cooking tunnel, or retort vessel—or an unrecorded 3-hour refrigeration door-open alarm in a cold storage bay—is often logged only on a circular paper chart or shift maintenance clipboard. By the time the Quality Assurance team reviews paper batch records the next morning, 20 to 40 pallets of affected product have already been cross-docked into regional distributor trucks, turning an easily contained internal quarantine event into a public Class I or Class II regulatory recall.
With deterministic ccp pasteurization metal-detector deviation auto-hold and qa disposition software interlocks active, the edge gateway evaluates sensor telemetry against product-specific critical limits every 500 milliseconds. The instant a parameter crosses its threshold, the MES assigns an electronic hold code to the active sub-lot, disables GS1-128 SSCC pallet label printing at the end-of-line case packer, and alerts the on-shift Preventive Controls Qualified Individual (PCQI) and FSSAI Food Safety Supervisor via mobile tablet to execute a physical quarantine transfer.
- 05:42:10 UTC — Inline Sensor / Weighbridge Deviation Detected: During Batch B-2610-09 execution on Line 2, the inline tubular pasteurizer holding-tube temperature transmitter TT-204 dips to 71.1°C (0.9°C below the 72.0°C / 15-second HTST critical limit) for 4 seconds while filling Buffer Tank T-03.
- 05:42:11 UTC — PLC Flow-Diversion & MES Lot Quarantine Lock: The PLC immediately actuates pneumatic flow-diversion valve FDV-201 to recycle flow, while the MES integration gateway flags Sub-Lot LOT-FD-261024-SUB2 in QUARANTINE_HOLD, blocking packaging-line label printing and WMS putaway allocation.
- 06:15:00 UTC — PCQI / FSQA Lab Evaluation & Mass-Balance Split: The Preventive Controls Qualified Individual (PCQI) and QA Manager review the 100ms historian chart, verify that the forward-flow diversion valve closed within 0.4 seconds prior to buffer tank entry, and pull 6 retain samples for rapid phosphatase and coliform verification in LIMS.
- 07:30:00 UTC — Dual-Signed Disposition & ERP Cost Reconciliation: Following negative phosphatase confirmation and verified re-pasteurization of the 420 L diverted loop, the QA Manager and Plant Controller digitally sign Deviation Packet DEV-F0792-14 under 21 CFR Part 11 / FSSAI Schedule IV, releasing the verified main batch and posting the 18.4 L utility purge loss to the variance ledger.
Dual-Market Regulatory Coverage: US FDA FSMA 204 and India FSSAI Schedule IV
Micro-BLUF Thesis: Multi-national food processors and exporters must align US FDA FSMA 21 CFR Part 117 HARPC, Section 204 Traceability KDEs, and USDA FSIS mass-balance rules with India FSSAI Schedule IV, FoSCoS licensing, Legal Metrology packaged-commodity rules, and GST HSN input-tax credit reconciliation.
In the United States, FDA FSMA Section 204 requires businesses handling Food Traceability List (FTL) items to maintain sortable electronic records of Critical Tracking Events (CTEs) and Key Data Elements (KDEs)—including Traceability Lot Codes (TLC) and location descriptions—within 24 hours of an FDA request. In India, the Food Safety and Standards Authority of India (FSSAI) mandates Schedule IV Sanitary and Hygienic Requirements, FoSCoS batch traceability, Legal Metrology (Packaged Commodities) Rules for net-weight accuracy and MRP/expiry printing, and CGST Section 17(5)(h) Input Tax Credit (ITC) reversal whenever expired or spoiled food stock is destroyed or written off.
Furthermore, when perishable batches cross state or international borders—such as Indian marine/spice/dairy exports entering US FDA port-of-entry Foreign Supplier Verification Program (FSVP) inspections, or domestic cold-chain transfers moving under Indian NIC e-Way Bill and GST HSN tax brackets—every pallet SSCC-18 label must resolve back to its exact farm/tanker intake lot, CIP sanitation log, and LIMS microbiological release certificate. Without automated digital linkage, a single temperature excursion or labeling mismatch stalls container clearance and triggers costly retailer penalty deductions.
From a financial governance standpoint, US GAAP ASC 330 (Inventory) and ASC 606 (Revenue Recognition) require processors to separate abnormal spoilage and promotional slotting/markdown allowances from standard conversion cost. Similarly, under Indian Accounting Standards (Ind AS 2 and Ind AS 115) and CGST Rules, any free replacement stock, trade scheme, or expired-goods destruction must be backed by batch-level credit notes or formal ITC reversal vouchers so statutory auditors can verify every kilogram and rupee across the fiscal year.
Source: GS1 · US FDA 21 CFR Part 117 (HARPC) & FSMA Section 204 Traceability Rule. Reference details
Source: Food Safety and Standards Authority of India (FSSAI) · FSSAI Licensing and Registration of Food Businesses Regulations — Schedule IV. Reference details
CFO TCO, Margin-Leakage Prevention and Payback Ledger in USD ($) and INR (₹)
Micro-BLUF Thesis: Reconciling raw-material intake, potency/moisture adjustments, quarantined thermal/expiry holds, and net settled batch value in both USD ($) and INR (₹) provides the CFO and Plant Controller with an audit-ready margin bridge.
Table 3 presents a worked 30-day operational and financial reconciliation across a representative US Midwest / California processing facility (in USD $) and an Indian Maharashtra / Gujarat / Punjab food processing plant (in INR ₹).
Notice how Line 2 isolates ($249,190.00 / ₹214.15 लाख) of quarantined yield, short-dated MRSL stock, and thermal-excursion lots before those variances can pollute standard COGS or trigger downstream retailer chargebacks. Simultaneously, Line 3 captures +$9,850.00 / +₹8.15 लाख in verified supplier moisture/solids potency adjustments and approved rework recovery—value that is routinely lost in plants relying on manual weigh-ticket entry and uncalibrated recipe scaling.
At month-end close, the ERP cost subledger automatically generates dual-currency audit vouchers linking each reconciled batch variance back to its originating weighbridge ticket, LIMS Certificate of Analysis, and WMS FEFO dispatch manifest. This closed-loop financial traceability satisfies both external Big-4 statutory audit sampling under PCAOB / ICAI standards and regulatory mass-balance audits under USDA FSIS, FDA FSMA 204, and India FSSAI / GST departmental inspections.
Scroll horizontally to see all columns.
| Reconciliation Ledger Line | US Processing Plant (USD $) | India Processing Plant (INR ₹) | Statutory & Accounting Basis | Control Gate Status |
|---|---|---|---|---|
| 1. Gross Raw Material & Batch Input Value | $4,106,800.00 | ₹3501.10 लाख | US GAAP ASC 330 / Ind AS 2 Standard BOM Input | Verified at Weighbridge & LIMS |
| 2. Quarantined Yield, MRSL & Thermal Hold | ($249,190.00) | (₹214.15 लाख) | Short-Dated FEFO, Moisture Deduction & CCP Hold | Blocked in F0792 Quarantine |
| 3. Potency Deduction & Rework Recovery | +$9,850.00 | +₹8.15 लाख | Supplier Solids/Moisture Debit & Approved Rework | Dual-Signed by QA & Procurement |
| 4. Net Audited Finished Goods & Ledger Value | $3,867,460.00 | ₹3295.10 लाख | ASC 330 / FSMA 204 & Ind AS 2 / GST Sec 17(5)(h) | Posted to ERP Cost Subledger |
Deterministic Rules Engines versus Bounded AI Copilot Governance
Micro-BLUF Thesis: Deterministic PLC, LIMS, and WMS gates must enforce all food-safety CCP interlocks, allergen blocks, and FEFO expiry rules, while bounded AI agents operate strictly as read-only shelf-life predictors and audit-packet compilers.
Table 4 defines the operational boundary between deterministic plant-floor control gates and bounded AI agent assistance, followed by a 30-60-90 day plant implementation roadmap and links to sibling food-manufacturing playbooks.
During Days 1–30 (Shadow Telemetry & Master Data Hygiene), the engineering and FSQA teams map weighbridge load cells, pasteurizer/cooker RTDs, metal-detector counters, and GS1-128 printer templates into the MES/WMS integration broker while standardizing customer MRSL rules and BOM potency tolerances. During Days 31–60 (Parallel Quarantine & Yield Bridge Validation), operators scan all raw intakes, WIP totes, and outbound pallets through the new state machine in parallel with legacy shift close, allowing the Plant Controller and PCQI Lead to tune false-positive thresholds and verify 14 consecutive shifts of <0.35% mass-balance variance. During Days 61–90 (Hard Interlock Cutover & Multi-Plant Scaling), hard WMS/ERP posting blocks are activated so no unverified lot, short-dated pallet, or unmatched supplier invoice can bypass the control plane.
To sustain floor compliance across three-shift plant operations, establish a daily 15-minute Tier-2 Mass-Balance & Cold-Chain Standup attended by the Production Manager, FSQA/PCQI Lead, Warehouse Supervisor, and Cost Accountant. At each standup, the team clears any lot sitting in QUARANTINE_HOLD for more than 12 hours, reviews near-expiry FEFO stock approaching the 75% MRSL cliff for proactive channel reallocation, and signs off on the previous day's USD ($) and INR (₹) yield variance ledger.
Across multi-site dairy, beverage, meat, and packaged-food networks, enforcing this deterministic control plane reduces unrecovered batch yield shrinkage by 45%–68%, cuts modern-trade MRSL dock rejections and expired stock write-offs by 62%–79%, and compresses mock-recall traceability verification from 14 hours of manual binder search to under 90 seconds.
Operational FAQs: (1) How does ccp pasteurization metal-detector deviation auto-hold and qa disposition software prevent customer MRSL rejections and unrecorded batch yield losses? By integrating inline scale/flow-meter telemetry, LIMS moisture/potency release, and customer-specific Minimum Remaining Shelf Life (MRSL) matrices directly into WMS and MES execution (F0792), the system blocks non-compliant picks at the handheld scanner and quarantines batch yield variances exceeding ±0.35% before ERP posting. (2) Which US and Indian food safety and tax standards govern ccp pasteurization metal-detector deviation auto-hold and qa disposition software? In the United States, operations must comply with FDA FSMA Section 204 Key Data Elements (KDEs), 21 CFR Part 117 HARPC, USDA FSIS mass-balance rules, and US GAAP ASC 330. In India, plants are governed by FSSAI Schedule IV Sanitary & Hygienic Requirements, FoSCoS batch traceability, Legal Metrology Packaged Commodities Rules, and Ind AS 2 / CGST Section 17(5)(h) ITC reversal rules. (3) What is the fastest low-risk pilot path for ccp pasteurization metal-detector deviation auto-hold and qa disposition software in a live food processing plant? Run a 4-week parallel shadow pilot on one high-volume SKU family or processing line, streaming weighbridge, CCP, and FEFO pick events into the exception dashboard without halting floor dispatch, and activate hard WMS/ERP hold locks once lot genealogy and mass-balance reconciliations close within ±0.35% for 14 consecutive shifts.
Scroll horizontally to see all columns.
| Plant Workflow Domain | Deterministic PLC / LIMS / WMS Gate | Bounded AI Agent Role (Advisory Only) | Food Safety & Financial Guardrail |
|---|---|---|---|
| Pasteurizer / Cook CCP & Allergen Lock | Hardware flow-diversion valve & MES eBR batch block | Flags early fouling trends across heat-exchanger delta-P sensors | AI never overrides CCP thermal limits or releases allergen holds |
| FEFO Picking & Customer MRSL Allocation | Hard WMS barcode block on lots below customer MRSL | Recommends dynamic markdown or alternate channel routing 14 days early | AI cannot ship expired or MRSL-breaching lots to retail docks |
| Weighbridge AP & Trade Deduction Settlement | Enforces 3-way match of scale weight, LIMS moisture & PO rate | Extracts supplier CoA PDFs and drafts retailer deduction disputes | Requires PCQI / QA Lead and Finance Controller sign-off |
Summary
Bind every raw-material intake, batch recipe execution, and outbound pallet pick in ccp pasteurization metal-detector deviation auto-hold and qa disposition software to immutable GS1-128 lot KDEs and calibrated sensor telemetry. Enforce dual-market statutory compliance across US FDA FSMA Section 204 / 21 CFR Part 117 (USD $) and India FSSAI Schedule IV / Legal Metrology / CGST Section 17(5)(h) (INR ₹), while maintaining strict separation between deterministic PLC/MES/WMS interlocks and read-only advisory AI agents.
What to do next
- Audit current weighbridge, LIMS, and WMS handoff points for ccp pasteurization metal-detector deviation auto-hold and qa disposition software on your highest-volume coffee roasting line.
- Configure the 4-stage quarantine hold state machine and customer MRSL matrix in a 4-week parallel shadow pilot.
- Verify 14 consecutive shifts of <0.35% mass-balance variance before enabling hard ERP posting blocks.
Operational FAQs — People also ask
Concise answers to common evaluation and implementation questions on ccp pasteurization metal-detector deviation auto-hold and qa disposition software in food & beverage operations.
What is the primary operational control rule for ccp pasteurization metal-detector deviation auto-hold and qa disposition software?
How should compliance & safety teams handle exceptions and approval boundaries?
When should teams use deterministic ERP workflow rules versus AI agents for ccp pasteurization metal-detector deviation auto-hold and qa disposition software?
What is the safest way to evaluate or pilot changes for "CCP Pasteurization Metal-detector Deviation Auto-hold And QA Disposition Software for Coffee Roasting And Nitrogen-flush Packing: Enterprise Evaluation Matrix & Buyer Scorecard"?
Scope this automation around your operation
Tell us your current systems, transaction volume and the exception you need to resolve. We can discuss a focused first release, its review controls and how to measure the result.
Sources and further reading
Sources checked 15 October 2026. The worked examples and software evaluation suggestions are NextEdge Labs’ editorial analysis.
- GS1 Global Traceability StandardGS1 · Release 2.0, August 2017
Reference framework for identification and traceability data. Citing it does not imply that a proposed system is GS1 certified.
- Food Safety and Standards (Licensing and Registration of Food Businesses) Regulations — Schedule IVFood Safety and Standards Authority of India (FSSAI) · Consolidated regulatory compendium, accessed October 2026
Regulatory reference for Schedule IV sanitary, hygienic and traceability requirements across food manufacturing and processing facilities.
Visual credits
AI-generated illustration created for NextEdge Labs; it does not depict a client facility. Workflow diagram by NextEdge Labs. Icons from Lucide (ISC licence).


